MCM Autotrack Conveyor Project For Automotive Components Manufacturer
16
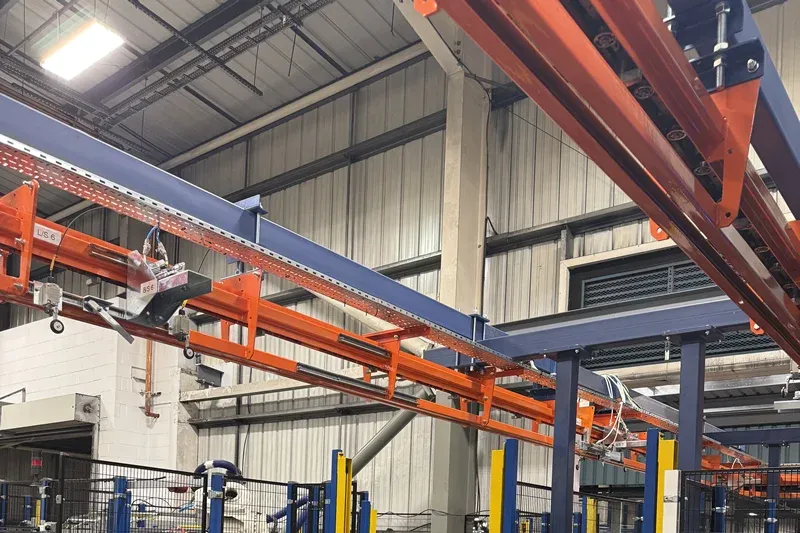
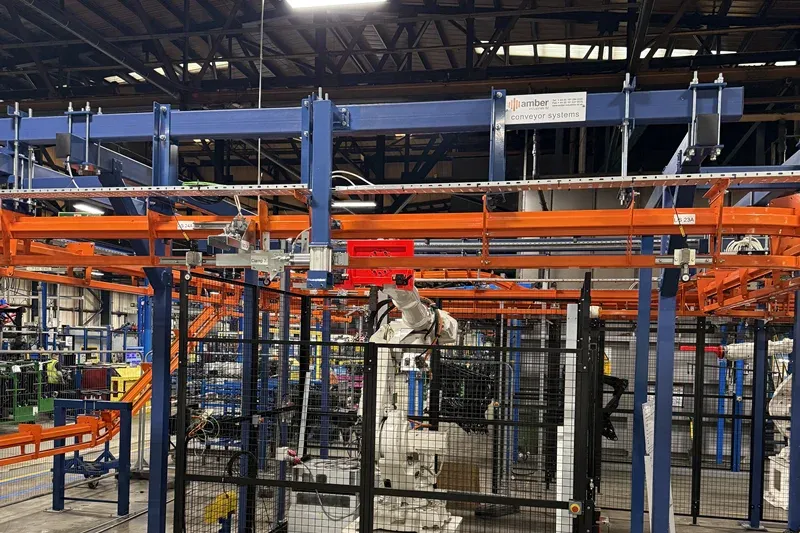
Amber Industries has successfully completed another conveyor systems project, supplying an MCM Autotrack Power & Free Overhead Conveyor System for a specialist automotive components manufacturer. The project demonstrates Amber Industries' continued expertise in delivering reliable and flexible materials handling solutions for the automotive manufacturing sector, where efficient product movement and streamlined production processes are essential.
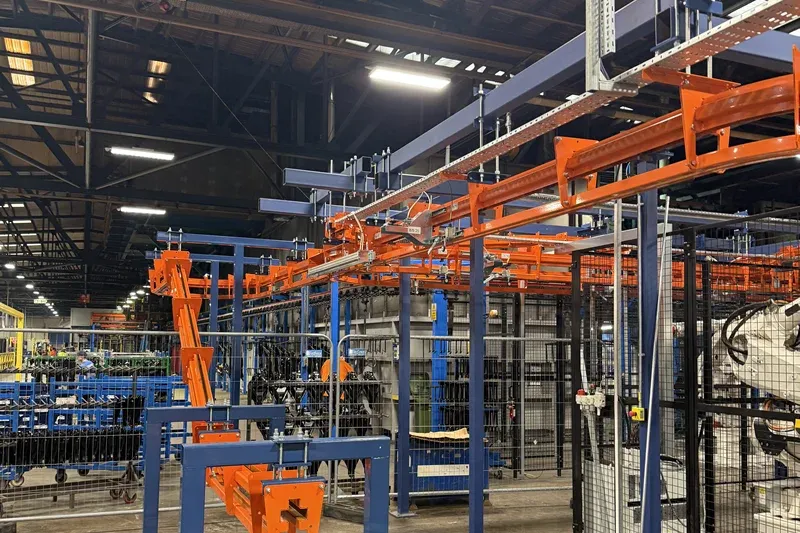
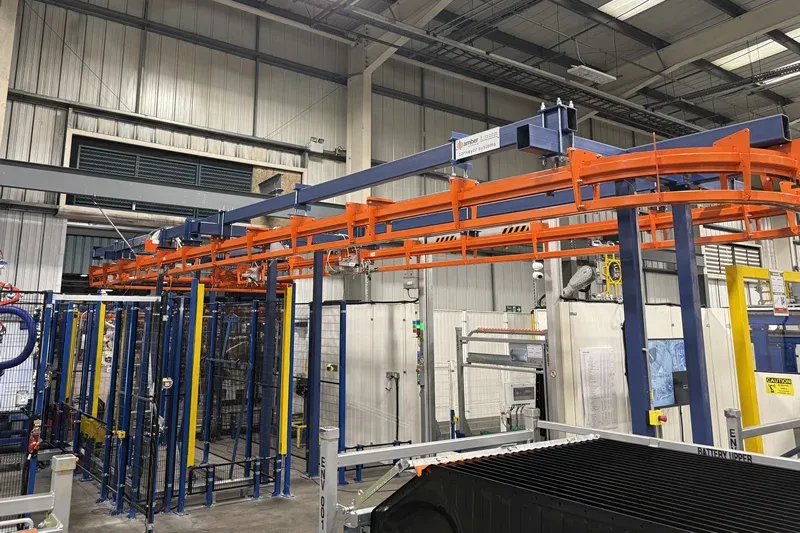
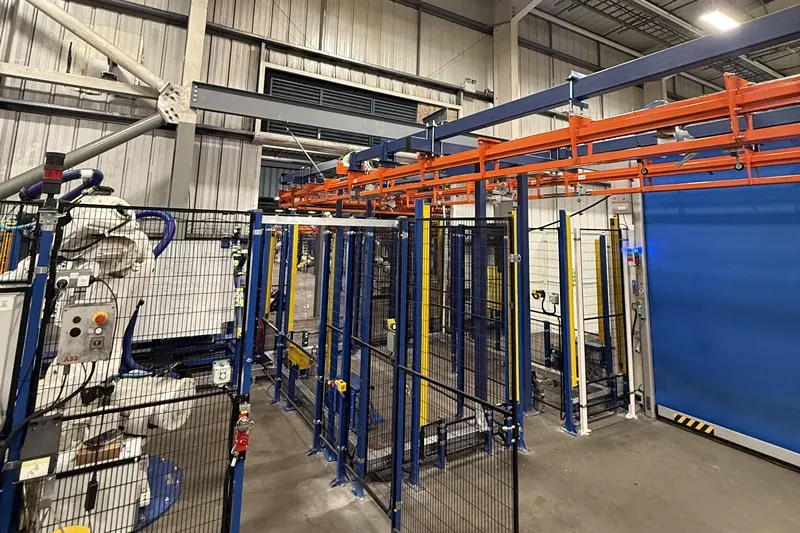
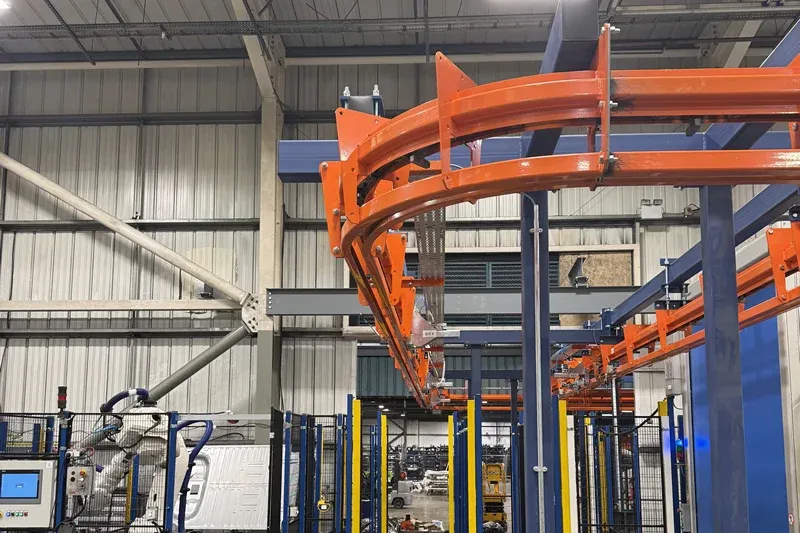
The MCM Autotrack system, developed by Amber Industries' MCM division, is designed to provide manufacturers with greater flexibility and control over the movement of components throughout the production environment. Unlike conventional overhead chain conveyors, the Autotrack Power & Free system incorporates separate powered chain and trolley tracks, allowing individual loads to be stopped, accumulated and directed through different stages of production as required. This flexibility makes the system particularly well suited to automotive manufacturing applications, where components may need to travel through multiple production, assembly, finishing and inspection processes.
Key benefits of the MCM Autotrack system include:
- Flexible Product Handling – Allowing components to be transported efficiently between different manufacturing operations.
- Controlled Product Movement – Enabling loads to be stopped and released independently to accommodate production requirements.
- Buffer Storage and Accumulation – Helping manufacturers manage variations in production flow and minimise disruption between processes.
- Automated Routing Capabilities – Providing the flexibility to direct products to different areas of the production facility.
- Improved Production Efficiency – Supporting a more organised and streamlined manufacturing process.
The completion of this latest project further highlights Amber Industries' experience in providing specialist overhead conveyor solutions to the automotive industry. With over 40 years of experience in conveyor engineering, Amber Industries continues to support manufacturers with innovative materials handling systems designed to meet the demands of modern production environments. Looking for a flexible overhead conveyor solution for your manufacturing facility? Discover more about our MCM Autotrack Power & Free Conveyor Systems.
Amber Industries Ltd is a UK-based engineering and manufacturing company specialising in the design, manufacture, installation and maintenance of industrial conveyor systems and automated materials-handling solutions. Headquartered in Oldham, Greater Manchester, the company has over 40 years of experience in conveyor technology, with business origins extending back more than 60 years. Its core proposition is to help manufacturers, warehouses and distribution businesses improve operational efficiency, reduce manual handling and optimise material flow through customised conveyor and automation solutions.
#AmberIndustries #MCMAutotrack #PowerAndFreeConveyors #OverheadConveyors #AutomotiveManufacturing #AutomotiveComponents #ConveyorSystems #MaterialHandling #ManufacturingAutomation #IndustrialAutomation #UKManufacturing #EngineeringSolutions
Other Articles
Amber Industries Delivers Conveyor Solution For Street Furniture Manufacturer
12
MCM Sidetrack Monorail Conveyor Systems – Heat Treatment
23
Amber Industries Puts Intelligent Control At The Heart of Conveyor Automation
21
MCM Freetrack Conveyor Systems Providing A Flexible Materials Handling Solution
4
MCM Dualtrack Inverted Conveyor System Delivers Stable & Precision Product Handling
9
Autotrack 500 Conveyor System Upgrade Phase 1 Shipped
26
MCM Sidetrack Monorail Conveyor Systems In Focus
7
That Is A Wrap On Paint Expo 2026
24
The Sidetrack 60 Encased For A Cleaner Smoother Operation
22
Come & Visit Amber Industries At Paint Expo 2026 In Hall 2 Stand 2242
14