What We Do
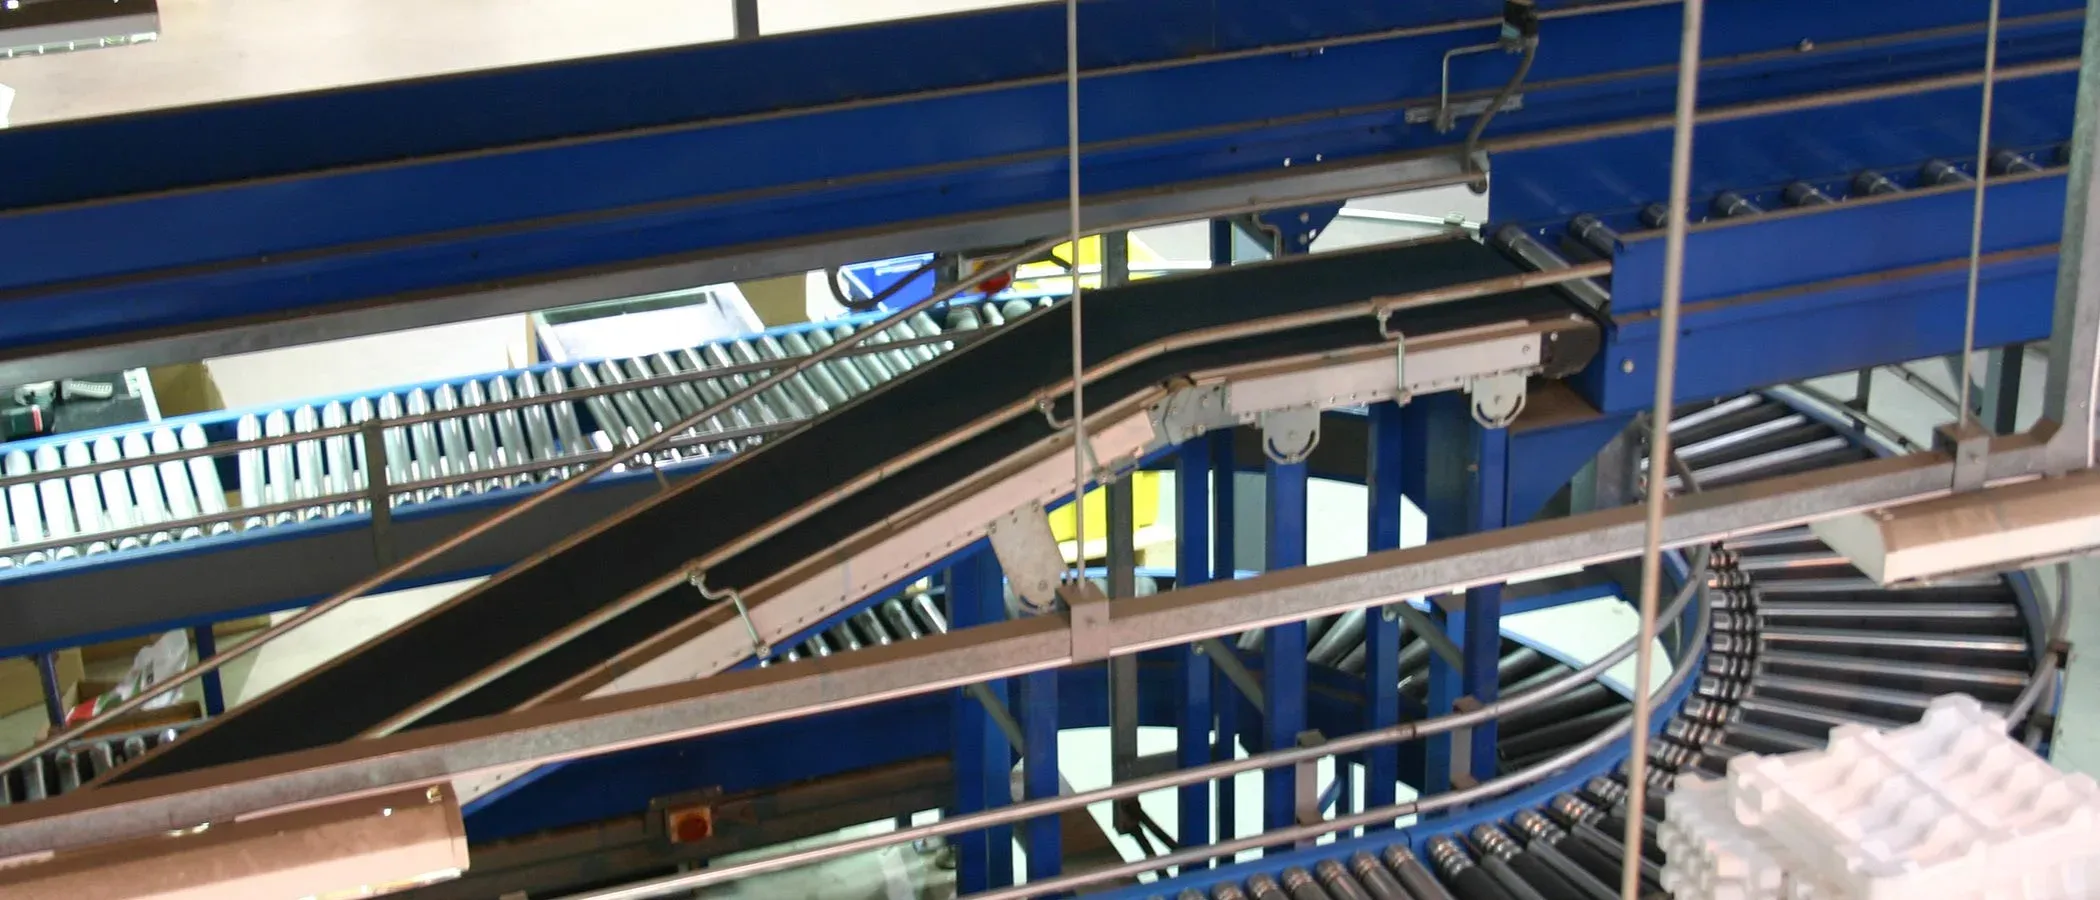
Amber Industries Ltd specialises in the design, manufacture, installation and maintenance of industrial conveyor systems and materials handling equipment. With over 40 years' experience in the conveyor industry, we provide practical, tailored solutions for manufacturers, warehouses, distribution centres and other businesses.
We recognise that no two materials handling operations are exactly alike. Our in-house engineering teams work closely with customers to understand their products, processes, available space and operational objectives before developing conveyor solutions suited to their requirements.
Our capabilities extend from initial concept development and detailed conveyor system design through to manufacture, installation, commissioning and operator training. We also provide ongoing maintenance, spare parts and technical support throughout the working life of the equipment.
Whether the requirement is for an individual conveyor, an extension to an existing installation or a complete turnkey materials handling system, our aim is to deliver reliable, efficient and cost-effective solutions.
Schedule of Conveyor System Services
Amber Industries offers a comprehensive range of conveyor engineering and project delivery services. Our multidisciplinary teams can support each stage of a project, from identifying the most suitable handling concept to maintaining the completed installation.
Concept Development
Conveyor systems often play a critical role in the efficiency, reliability and profitability of manufacturing and distribution operations. Understanding how products move through a facility is therefore an important first step in developing an effective materials handling solution.
We work closely with customers to assess their existing processes, identify handling challenges and understand the physical, operational and financial constraints of each project. Our engineering teams then develop potential conveyor concepts, drawing on our own equipment and, where appropriate, complementary technologies from other suppliers.
During concept development, we can:
- Prepare initial conveyor layouts, schematics and process flow diagrams.
- Assess product movement, handling requirements and system capacity.
- Develop preliminary equipment specifications and conceptual designs.
- Provide indicative project costs and support initial return-on-investment assessments.
- Consider future expansion, changes in production requirements and opportunities to adapt the system over time.
Conveyor System Design and Engineering
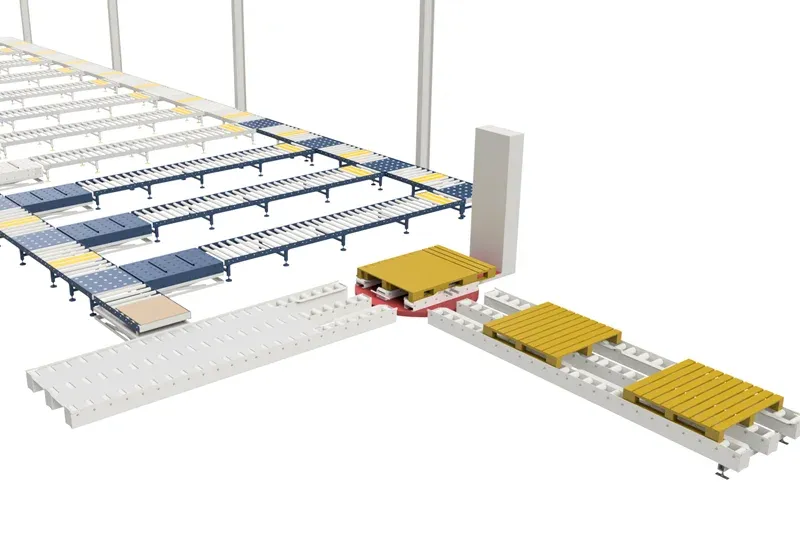
Once a suitable concept has been established, our specialist engineers develop the design in greater detail. This involves selecting appropriate conveyor technologies, planning equipment layouts and considering how individual conveyor sections will operate together within the customer's facility.
Our engineering capabilities include mechanical design, control systems engineering and the use of 2D and 3D computer-aided design (CAD) software. These resources support the development of bespoke conveyor equipment and integrated materials handling systems tailored to specific applications.
Design considerations may include product dimensions and weights, required handling speeds, available floor space, changes in elevation, access for operators and maintenance, and integration with existing equipment.
Our objective is to develop a practical conveyor arrangement that supports reliable product movement while making effective use of the available operating space.
Conveyor Manufacture and Assembly
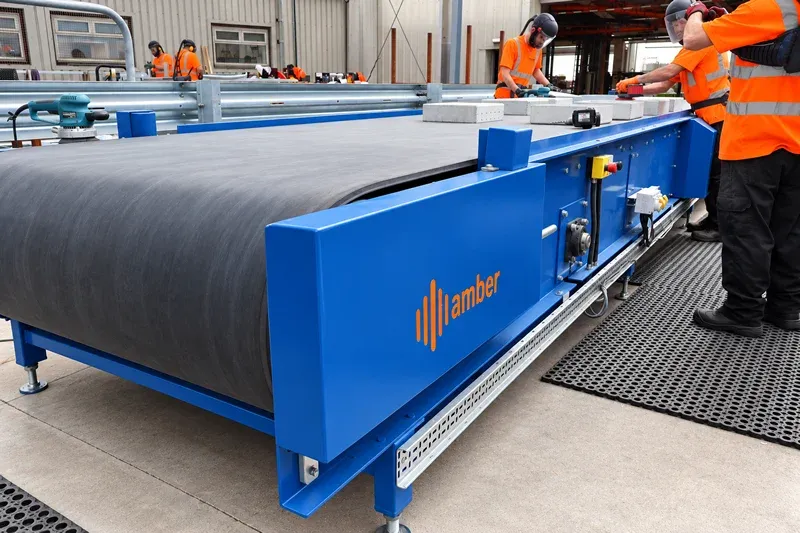
Amber Industries operates from a 2,000-square-metre manufacturing facility in Oldham, Greater Manchester, where our engineering, production and assembly activities are based.
Our in-house manufacturing capabilities enable us to produce conveyor equipment and associated mechanical handling solutions to suit individual project requirements. Bringing design, manufacture and assembly expertise together helps maintain coordination between the engineering and production stages of a project.
We supply conveyor equipment for a wide range of applications, from individual handling requirements to larger systems incorporating multiple conveyor technologies.
Installation and Commissioning
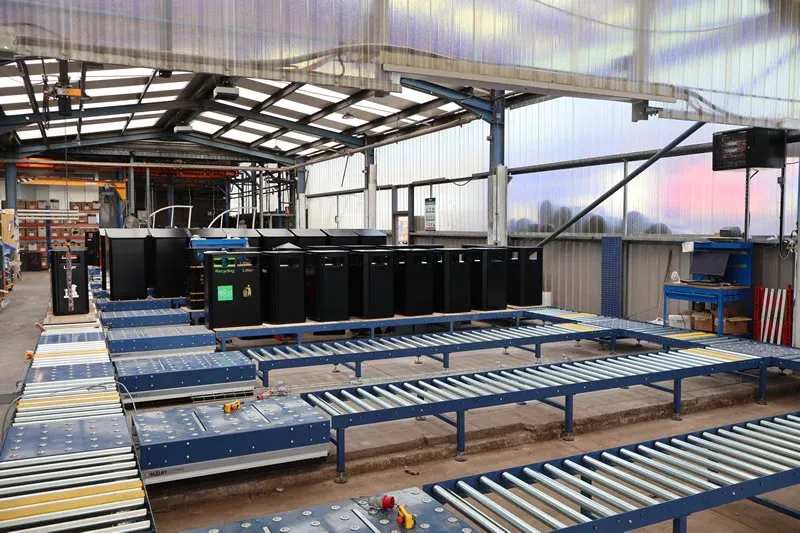
Our involvement can continue beyond manufacture to include conveyor system installation and commissioning at the customer's premises.
Our installation and commissioning engineers work to bring the conveyor equipment into operation, coordinating the installation of individual sections and checking that the completed system performs as intended.
For projects involving existing production or distribution facilities, careful installation planning is particularly important. We work with customers to understand site requirements and coordinate activities around the practical needs of their operations.
Operator Training and System Handover
Effective operation and maintenance are important considerations when introducing new conveyor equipment.
As part of a turnkey project, Amber Industries can provide operator training and support during system handover, helping customer personnel become familiar with the equipment and its intended operation.
By supporting customers through the transition from installation to day-to-day use, we aim to help them gain the full operational benefit of their conveyor investment.
Conveyor Maintenance, Spare Parts and Ongoing Support
Our commitment to customers does not end when a conveyor system is installed. Amber Industries also provides maintenance, spare parts and technical support to help keep conveyor equipment operating reliably throughout its service life.
Planned servicing, replacement components and appropriate maintenance support can help businesses manage equipment wear, reduce the risk of unexpected interruptions and maintain efficient materials handling operations.
Learn more about our conveyor spares and services.
Our Conveyor Systems and Materials Handling Solutions
Amber Industries offers a broad range of conveyor technologies and specialist handling solutions. The most appropriate equipment depends on the products being transported, the operating environment and the requirements of the wider manufacturing or distribution process.
Our main product and service areas include:
- Overhead Conveyors – Conveyor systems designed to transport products above floor level, helping businesses make effective use of available space and support manufacturing and handling operations.
- Floor Conveyors – Conveyor equipment for moving products, cartons, totes, pallets and other loads through production, warehousing and distribution environments.
- Powered Belt Curves – Specialist conveyor bends designed to transfer products smoothly around changes in direction within a conveyor system.
- Bespoke Handling Solutions – Custom-designed equipment and integrated conveyor arrangements developed for applications where standard products may not fully meet operational requirements.
- Spares and Services – Conveyor maintenance, replacement parts and technical support for new and existing equipment.
Our engineering teams can also combine different conveyor technologies within a single installation to address more complex materials handling requirements.
Conveyor Systems for Manufacturing, Warehousing and Distribution
Reliable conveyor systems help businesses move materials and products between different stages of their operations. Depending on the application, conveyors can support production processes, assembly activities, product transfers, packaging, order fulfilment and distribution.
Amber Industries works with customers across a variety of industrial sectors, developing solutions around the practical demands of their facilities. These may include handling different product types, working within restricted spaces, connecting existing equipment or planning for future changes in operational requirements.
By combining mechanical engineering, conveyor technology and project delivery expertise, we aim to provide systems that support efficient material flow and reduce unnecessary manual handling.
Our Conveyor System Projects
Our experience includes conveyor projects for a range of manufacturing and materials handling applications. Each installation presents its own requirements, from the types of products being transported to the layout and operational demands of the facility.
For examples of how Amber Industries has approached real-world conveyor and materials handling challenges, explore our conveyor system case studies.