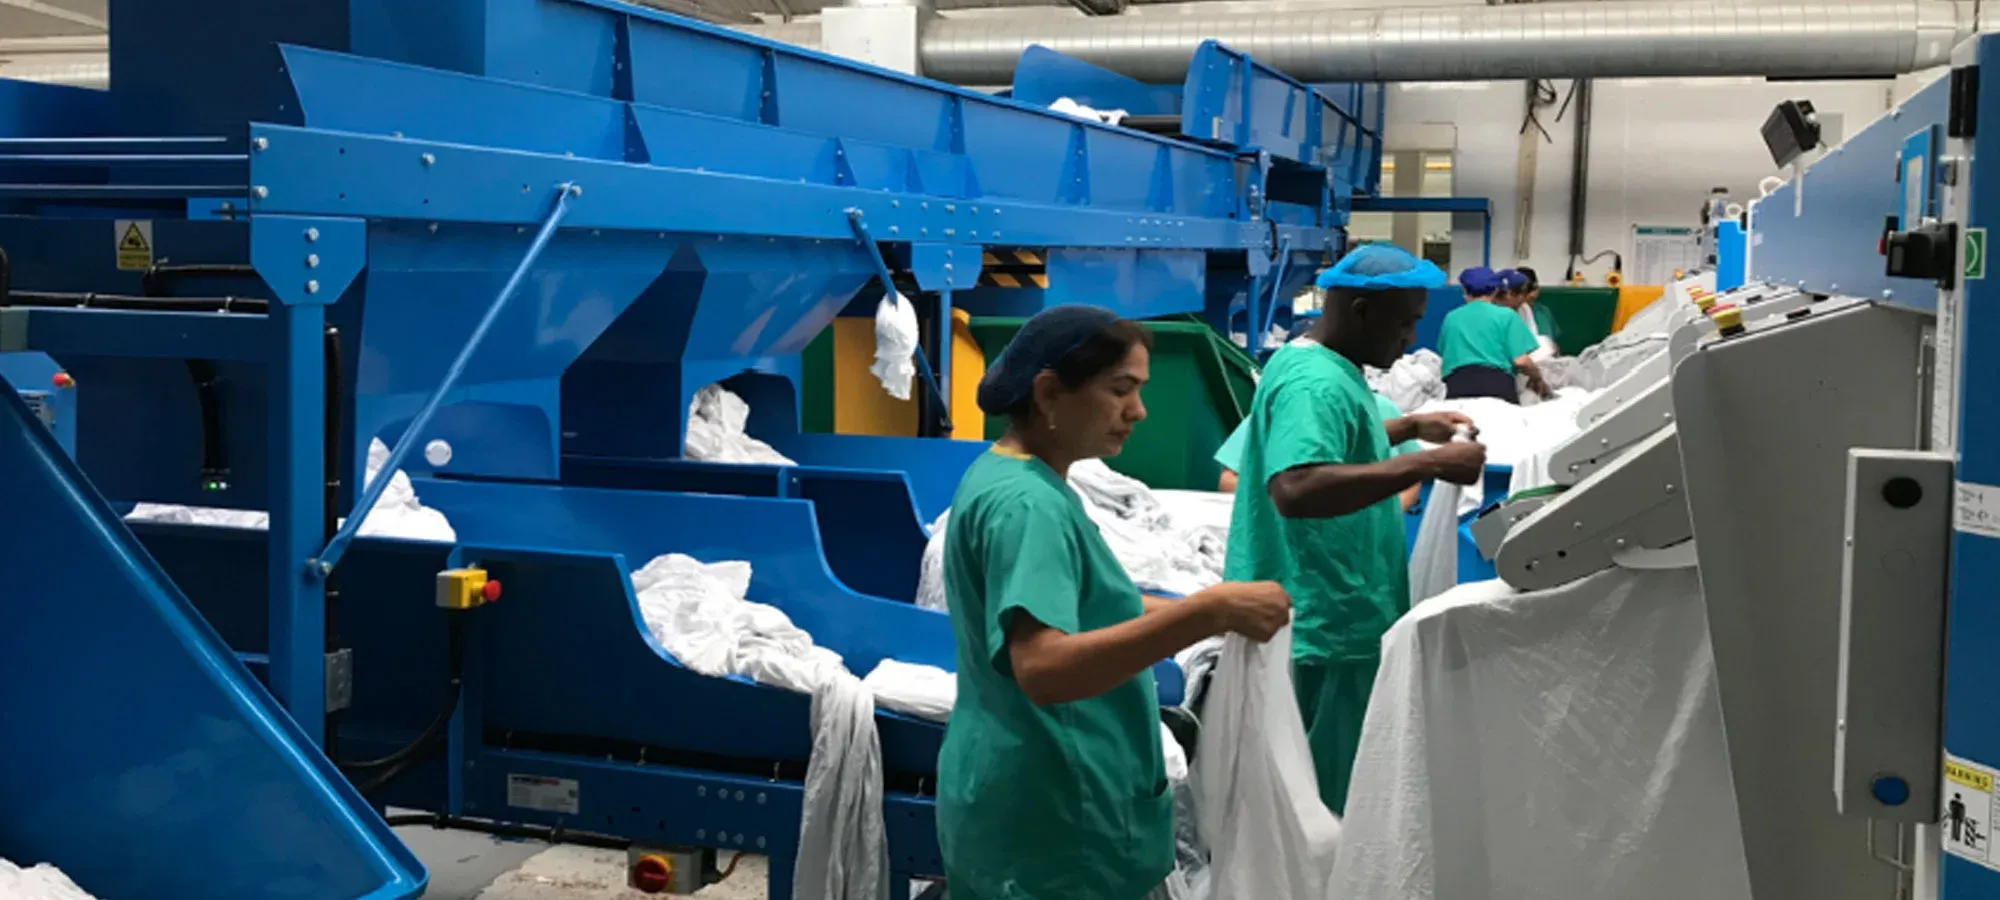
Amber Industries designs and manufactures bespoke conveyor systems for commercial and industrial laundries, providing specialist solutions for moving, sorting and transferring linen throughout the laundry process.
Our engineering team develops equipment to address specific handling challenges, minimise snagging and make effective use of available space.
Examples include:
Recirculating Linen on Sorting Platforms
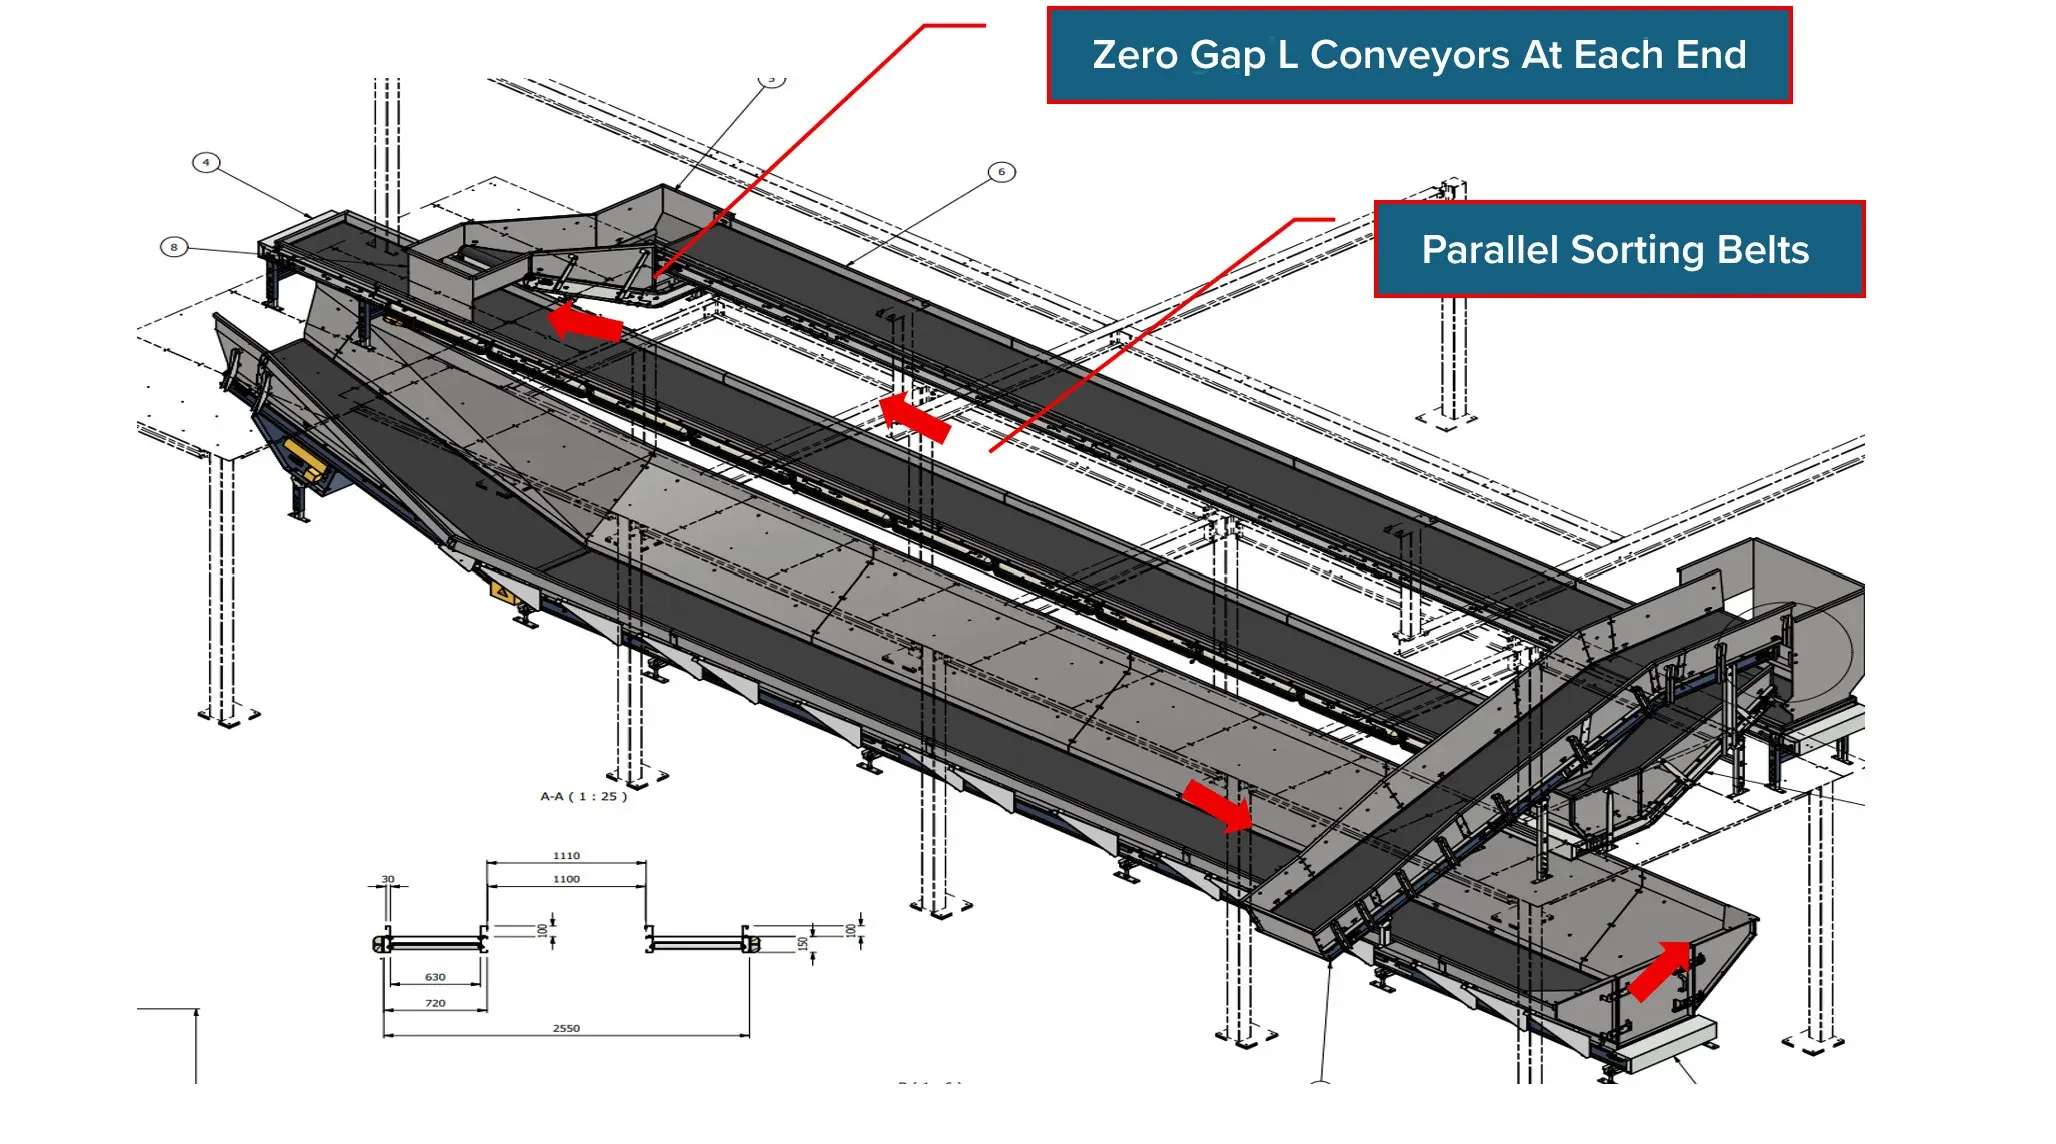
Parallel sorting conveyors can be arranged to recirculate loose linen around sorting platforms without requiring excessive floor space. These systems require careful design at the cross-transfer sections at each end of the conveyor arrangement.
Amber Industries pays particular attention to these transfer points to support the efficient movement of linen and minimise the risk of snagging and frequent jams.
Zero-Gap L-Shaped Laundry Transfer Conveyors
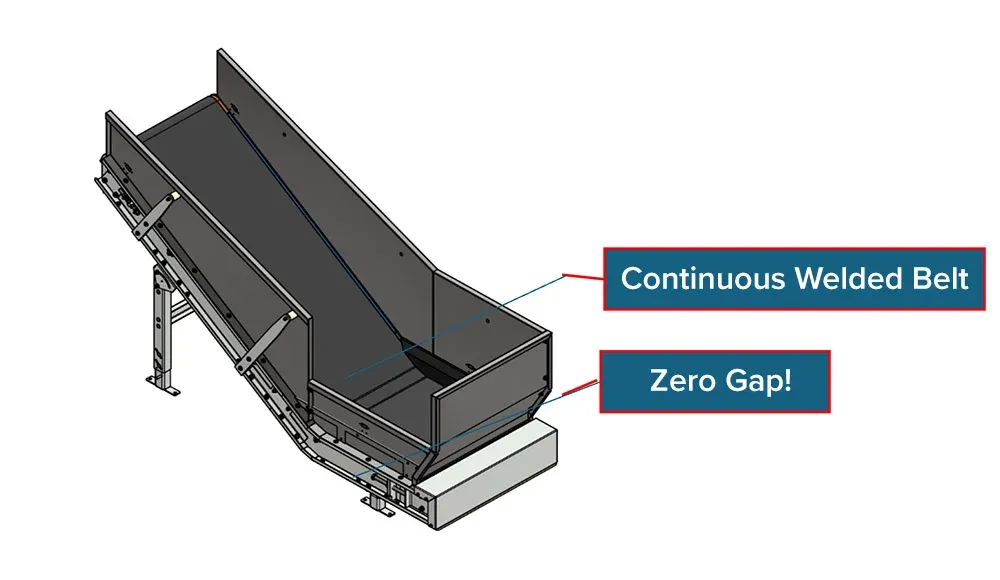
Zero-gap L-shaped conveyors provide a reliable way to transfer linen between parallel sorting belts. Their design eliminates the gap traditionally found between the belts of the horizontal and inclined conveyor sections.
Removing this gap helps reduce the risk of linen tags becoming trapped or snagged between rollers. It also eliminates finger-trap points at the base of the incline, improving safety and supporting more efficient linen handling.
Overhead Shuttle Conveyors for Feeding Multiple Ironers
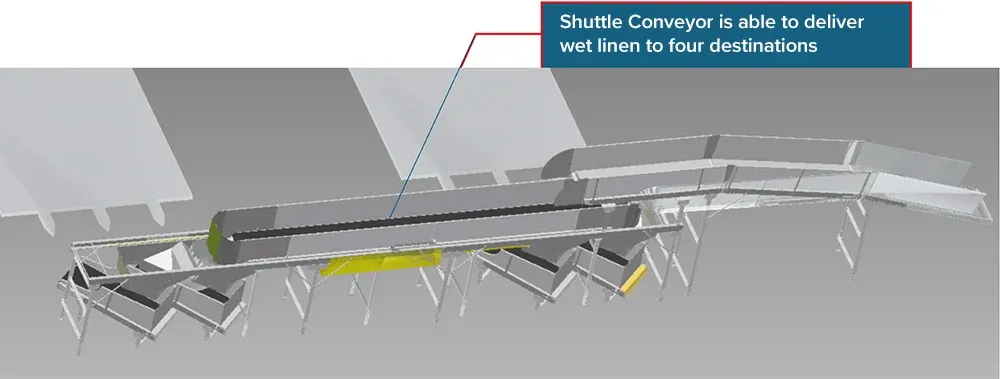
Feeding wet linen to multiple ironers can require considerable floor space. Amber Industries has developed a ceiling-mounted shuttle conveyor system that uses overhead space to transfer wet linen to up to four individual ironers.
The shuttle conveyor is designed to accommodate a full 80 kg load of wet linen directly from the cake breaker. It transfers the linen to one of four buffer conveyors, where operators can pick individual items for feeding into the ironers.
During transfer, the linen load is spread along the length of the shuttle conveyor, helping to break up the load. The arrangement also provides a substantial drop between conveyors, reducing potential snagging and jamming points.
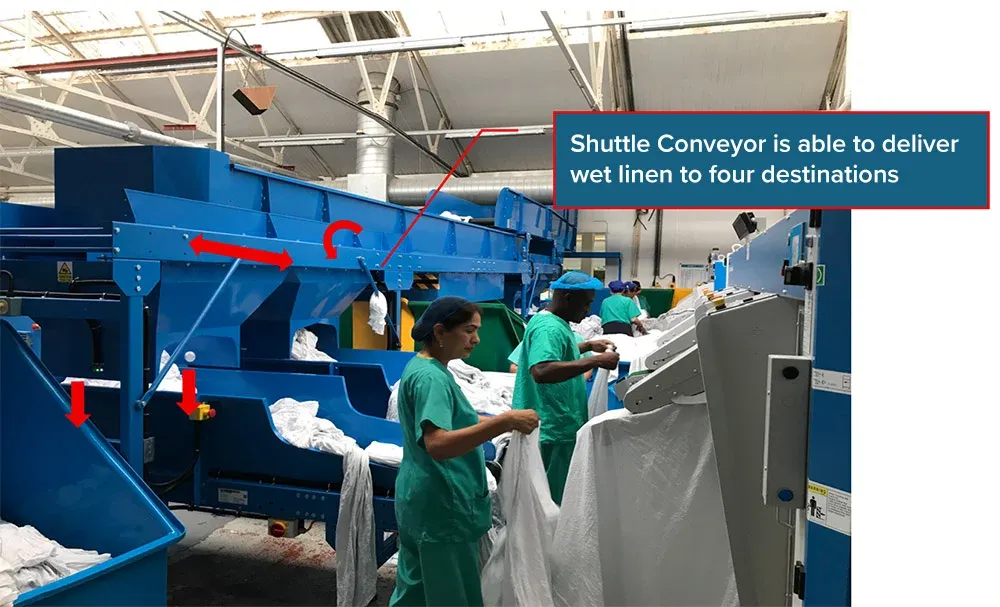
Sliding shuttle conveyor feeding four ironers
Space-Saving Turntable Conveyors for Wet Linen Cakes
Moving wet linen cakes weighing 80, 90 or 100 kg between a cake press and cake breakers can be challenging, particularly in older laundry buildings where access restrictions and obstructions create complex conveyor routes.
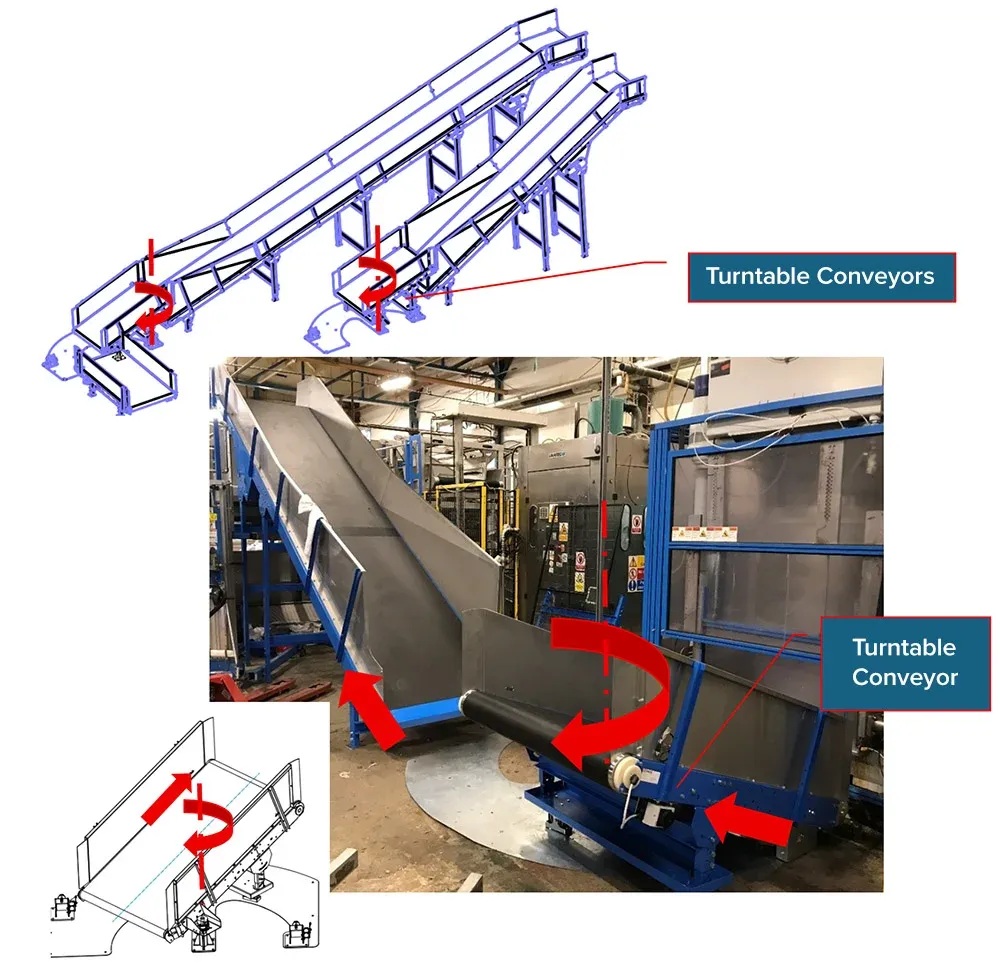
Amber Industries offers a specialist motorised turntable belt conveyor designed to overcome these handling challenges. The system consists of a horizontal or inclined belt conveyor, often only slightly longer than the linen cake itself, mounted on a motorised turntable.
The turntable allows the conveyor to change direction while occupying less floor space than some conventional arrangements, such as belt bends. Where required, an inclined configuration can also raise the linen cake as it turns, providing a useful solution when the destination is above floor level and there is insufficient space for a separate elevator.
An additional benefit of the inclined arrangement is that the linen cake can drop over a waterfall transfer as it leaves the turntable, helping to break up the compressed linen before the next stage of processing.
Frequently Asked Questions About Bespoke Laundry Conveyors
Standard laundry conveyors are generally designed for common material handling tasks, such as transporting linen between processing areas. Bespoke laundry conveyors are engineered to meet more specific operational requirements, particularly where space restrictions, unusual transfer arrangements or existing machinery make a conventional system unsuitable.
Amber Industries designs bespoke solutions such as overhead shuttle conveyors, zero-gap transfers, recirculating sorting systems and motorised turntable conveyors for challenging laundry environments.
Loose linen and attached tags can become trapped at conveyor transfer points, particularly where gaps exist between adjoining conveyor sections.
Amber Industries designs specialist transfer arrangements, including zero-gap L-shaped conveyors, to minimise these problems. Careful attention to the cross-transfer sections of recirculating sorting conveyors also helps linen move efficiently through the system.
A zero-gap laundry conveyor eliminates the gap traditionally found between the horizontal and inclined belt sections of certain transfer conveyors.
This design helps prevent loose linen and tags from becoming trapped between rollers. It also removes finger-trap points at the base of the incline, improving safety and reducing potential causes of conveyor stoppages.
Yes. Amber Industries has developed a ceiling-mounted shuttle conveyor system capable of distributing wet linen to up to four individual ironers.
The shuttle can accommodate an 80 kg load directly from a cake breaker and transfer linen to one of four buffer conveyors, where operators collect individual items for feeding into the ironers.
Using overhead space also reduces the amount of floor area required for this part of the laundry operation.
Bespoke conveyor arrangements can make better use of available space by moving equipment overhead or allowing loads to change direction within a compact area.
Amber Industries has developed ceiling-mounted shuttle conveyors for feeding ironers and motorised turntable conveyors for moving wet linen cakes through restricted layouts.
These approaches are particularly useful in older laundry buildings where existing machinery, structural features or access routes limit the space available for conventional conveyor systems.
A motorised turntable conveyor can be used to move heavy, compressed cakes of wet linen between a cake press and cake breakers, particularly where the conveyor route must change direction within a restricted space.
Amber Industries' design uses a horizontal or inclined belt conveyor mounted on a motorised turntable. It can handle applications involving wet linen cakes weighing 80, 90 or 100 kg, depending on the system design.
An inclined arrangement can also raise the cake while turning and allow it to drop at the discharge point, helping to break up the compressed linen.
Yes. Amber Industries develops bespoke laundry handling solutions to address the requirements of individual installations.
The conveyor arrangement can be designed around factors such as available floor space, existing processing machinery, transfer heights, linen handling requirements and the route products need to follow.
Examples include overhead shuttle conveyors for multiple ironers, recirculating linen sorting systems and turntable conveyors for restricted spaces.