Weir Valves - Overhead Conveyor
MCM Autotrack 500 Power & Free Overhead Conveyor System for Weir Valves
Weir Valves & Controls UK Ltd approached MCM Conveyors, a division of Amber Industries, to improve the efficiency and handling capacity of its valve finishing operation. The project required an overhead conveyor system capable of transporting heavy valves through shot blasting, spray painting and oven curing processes.
Following a competitive tender process, MCM was appointed to provide a complete handling solution. Philip Dollin of Weir Valves & Controls UK Ltd commented:
"After reviewing a number of tender proposals, overhead conveyor specialist MCM Conveyors was appointed to provide a total handling solution. Apart from being competitive, MCM Conveyors clearly demonstrated that they understood our requirements and could also offer comprehensive after sales service, which we believe is essential in committing to capital investment projects."
Autotrack 500 Power & Free Conveyor System
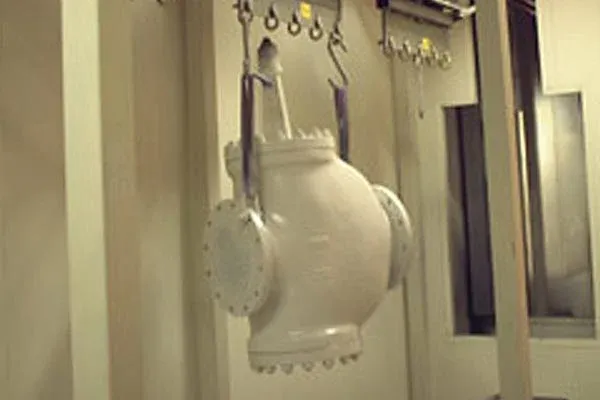
The system was designed to provide maximum flexibility and efficiency when handling individual valves weighing up to 2,000 kg. Products are suspended from bespoke rotating, multi-jig flightbars carried by an MCM Autotrack 500 (AT500) power and free overhead conveyor. The system transports valves around a circuit to designated unloading and finishing stations.
At the loading station, an operator uses a pendant raise/lower control to lower the carriage to an ergonomic working height, allowing slings to be attached to the valve. Data is assigned to each loadbar assembly through an electronic tag, which is used at the paint booth and curing oven to determine product routing, paint finish and curing times.
Once the slings are secured and the valve has been masked, the operator raises the drop-section carriage. The final 200 mm of vertical travel is completed automatically under PLC control, which monitors movement and system functions. A release button then allows the loaded flightbar to travel towards the shot blasting area, where it accumulates until required. An empty loadbar assembly can then enter the loading and unloading station.
Automated Shot Blasting and Paint Finishing
A product load gate provides a safety check to ensure that each valve remains within the permitted work envelope. If an oversized or misaligned load is detected, the overhead conveyor generates an alarm and stops.
The PLC detects when an empty position is available within the shot blasting enclosure. Once an operator activates the product call button, the loadbar assembly enters the enclosure. Following shot blasting, the operator activates the product release button, automatically opening the machine doors and allowing the valve to travel towards the paint booth.
Within the paint booth conveyor section, the multi-jig flightbar can be unlocked using a push-button control, allowing the operator to rotate the valve during painting. Once painting is complete, the flightbar is locked back into its inline position on the overhead conveyor.
A specially designed guide helps reorientate and lock the rotating flightbar if the operator has not completed this procedure. If the flightbar remains misaligned beyond the permitted angle, a load gate detects the condition, triggers an alarm and stops the conveyor.
The Read/Write electronic tagging system provides operators with process information, including paint colour, the number of coats required and curing times. Additional information can also be assigned to individual loadbar assemblies by Weir Valves & Controls. All controls and activation buttons within the booth enclosures are intrinsically safe.
Oven Curing and Automated Product Routing
After painting, the valves accumulate on the overhead conveyor. A switch gate directs products onto different conveyor lines according to their required curing times of three or six hours before they pass through the oven.
After curing, the separate conveyor lines merge. Valves requiring additional painting are recirculated through the system, while completed products are automatically routed towards the loading and unloading station, where they are lowered onto waiting pallets. The empty flightbars can then be reloaded to begin another painting cycle.
Overhead Conveyor Installation, Training and Maintenance
Following installation, Weir Valves & Controls UK Ltd reported that the system was operating reliably. MCM also provided operator training and guidance on basic maintenance procedures. The customer subsequently appointed MCM to provide scheduled overhead conveyor maintenance and servicing.
Weir Valves & Controls UK Ltd commented:
"MCM Conveyors worked very closely with our Project Team and we developed a good working relationship. MCM's commitment in delivering this project could not be faulted and the installation was completed on time and within budget. Once installed, MCM provided operative training for our people and highlighted basic maintenance procedures. It was important that the line offered maximum flexibility to complete valve painting to customers specific individual requirements. The system has operated successfully and reliably since installed and Weir Valves & Controls UK appointed MCM to provide an ongoing scheduled service and maintenance package. As a result of this success, and based on the above experience I would not hesitate to recommend them".