Amber Industries Supports Specialist UK Manufacturer With Conveyor Maintenance Contract
22
Amber Industries is pleased to be providing a comprehensive conveyor servicing and maintenance contract for a specialist UK manufacturer of bespoke steel and aluminium doors and physical security solutions. The customer designs and manufactures a wide range of high-quality products, including security doors, fire-rated doors, acoustic doors, flood-resistant doors, security grilles and access control systems. Serving commercial, industrial and residential markets, the company places a strong emphasis on safety, security, durability and compliance with recognised industry standards.
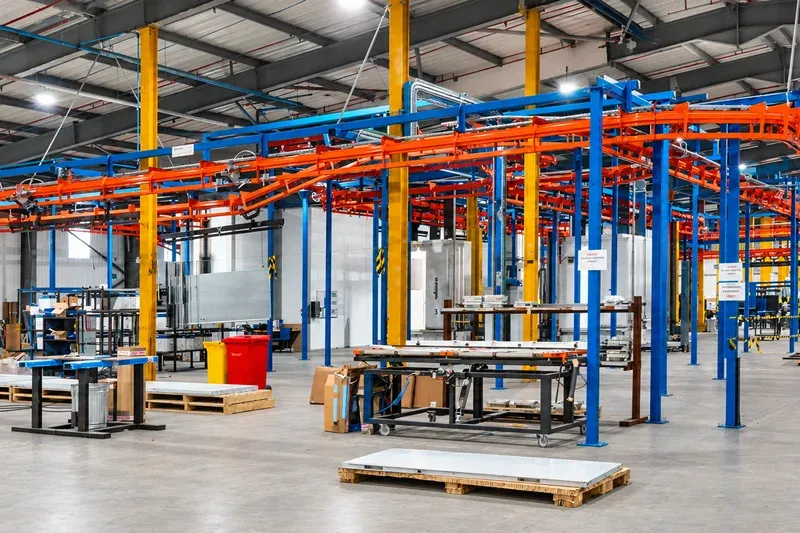
Planned Overhead Conveyor Servicing and Maintenance
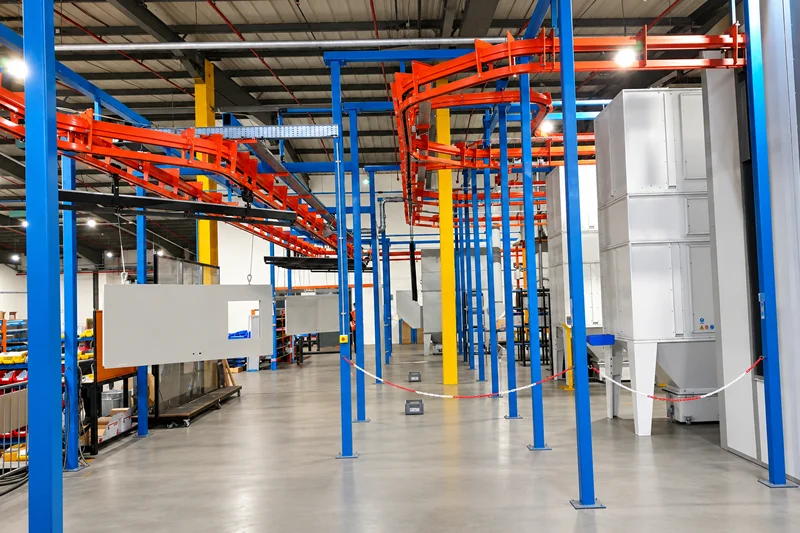
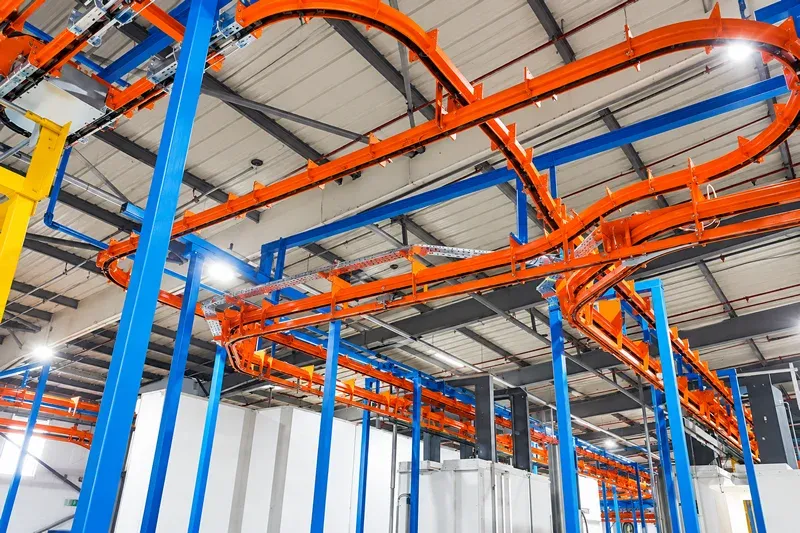
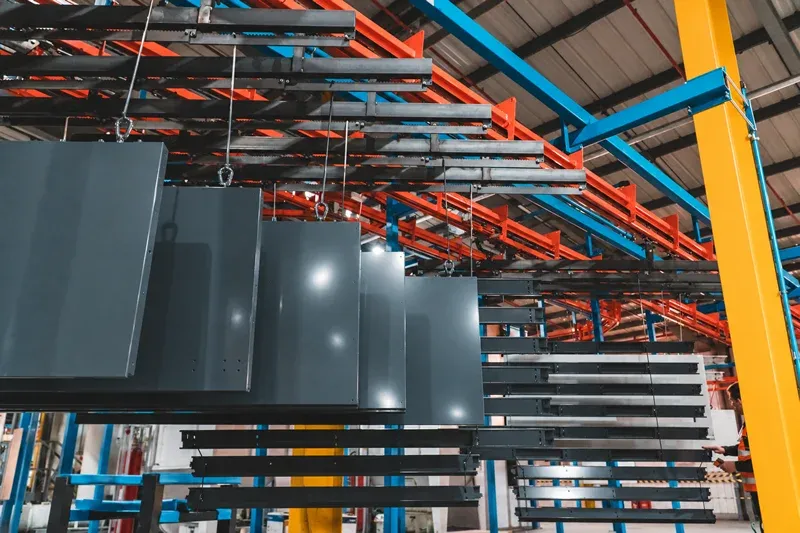
To help maintain the reliability and performance of its production operations, Amber Industries is providing a twice-yearly service contract for the customer's overhead conveyor system, including drop sections. As part of the agreement, two experienced Amber Industries engineers will carry out scheduled service visits twice a year, conducting thorough inspections of key conveyor components, including:
- Drive units and track
- Conveyor chain and loadbars
- Blade stops and switch points
- Trolleys and drop sections
Following each visit, the customer will receive a detailed written report outlining the findings and any recommended maintenance actions. The contract also includes 24-hour telephone support, providing additional reassurance and access to technical assistance when required.
By delivering regular preventative maintenance and specialist engineering support, Amber Industries aims to help the customer minimise unexpected downtime, maintain operational efficiency and extend the working life of its conveyor equipment. Keeping production moving with reliable conveyor servicing and expert engineering support.
About Amber Industries
Amber Industries Ltd is a UK-based engineering and manufacturing company specialising in the design, manufacture, installation and maintenance of industrial conveyor systems and automated materials-handling solutions. Headquartered in Oldham, Greater Manchester, the company has over 40 years of experience in conveyor technology, with business origins extending back more than 60 years. Its core proposition is to help manufacturers, warehouses and distribution businesses improve operational efficiency, reduce manual handling and optimise material flow through customised conveyor and automation solutions.
#AmberIndustries #ConveyorMaintenance #ConveyorServicing #OverheadConveyors #PreventativeMaintenance #EngineeringSupport #UKManufacturing #ManufacturingIndustry #IndustrialMaintenance #MaterialHandling #ProductionEfficiency #ConveyorSystems
Other Articles
MCM Autotrack Conveyor Project For Automotive Components Manufacturer
16
Amber Industries Delivers Conveyor Solution For Street Furniture Manufacturer
12
MCM Sidetrack Monorail Conveyor Systems – Heat Treatment
23
Amber Industries Puts Intelligent Control At The Heart of Conveyor Automation
21
MCM Freetrack Conveyor Systems Providing A Flexible Materials Handling Solution
4
MCM Dualtrack Inverted Conveyor System Delivers Stable & Precision Product Handling
9
Autotrack 500 Conveyor System Upgrade Phase 1 Shipped
26
MCM Sidetrack Monorail Conveyor Systems In Focus
7
That Is A Wrap On Paint Expo 2026
24
The Sidetrack 60 Encased For A Cleaner Smoother Operation
22