Our Conveyor System Case Studies
Discover how Amber Industries approaches real-world conveyor engineering and materials handling challenges. Our case studies showcase a selection of projects involving conveyor system design, manufacture, installation and integration.
From individual conveyor installations to more complex handling systems, each project reflects the practical requirements of the customer's operation. Explore our case studies below to see examples of the conveyor solutions we have delivered.
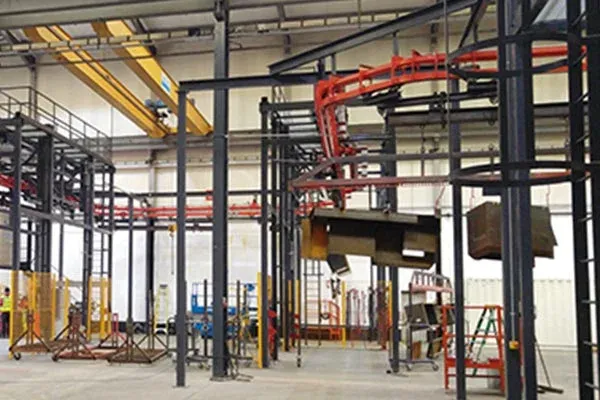
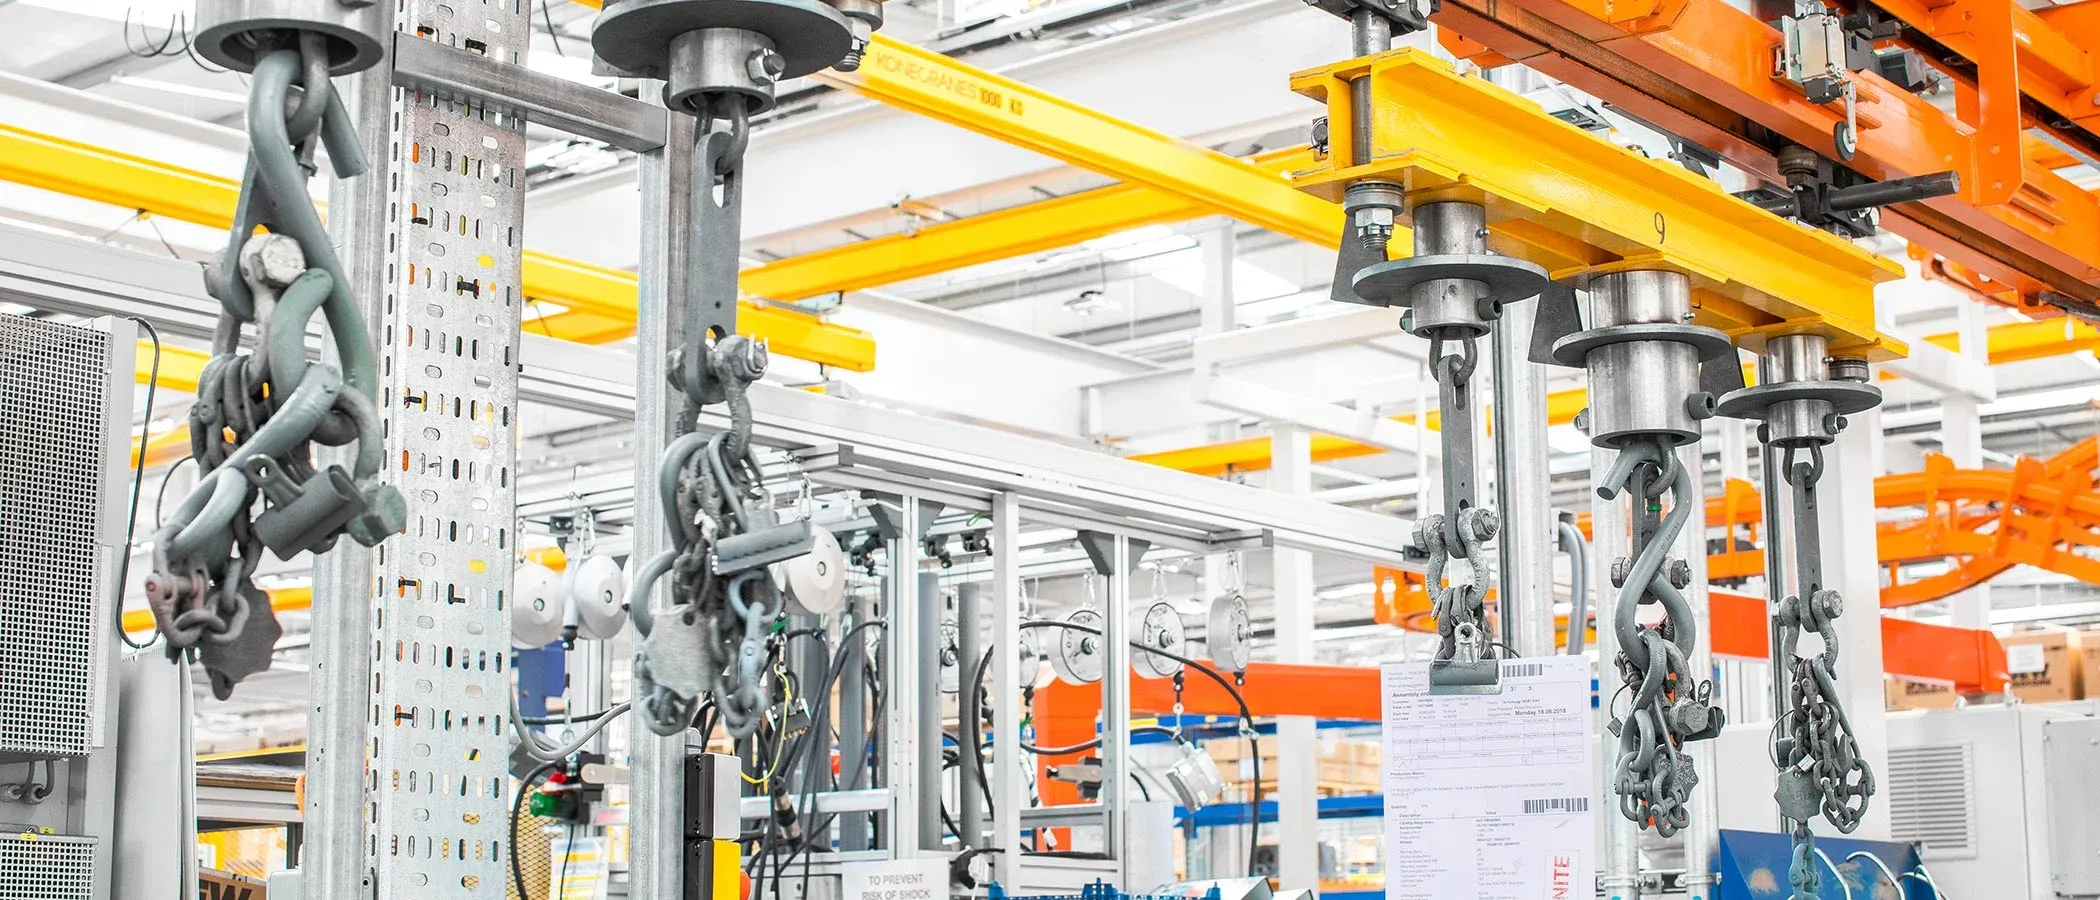
SEW Eurodrive - Overhead Conveyor
Discover how Amber Industries supplied an MCM Autotrack power and free overhead conveyor system for SEW Eurodrive's paint plant in West Yorkshire, incorporating automated routing and a dedicated Fast Track lane for urgent orders.
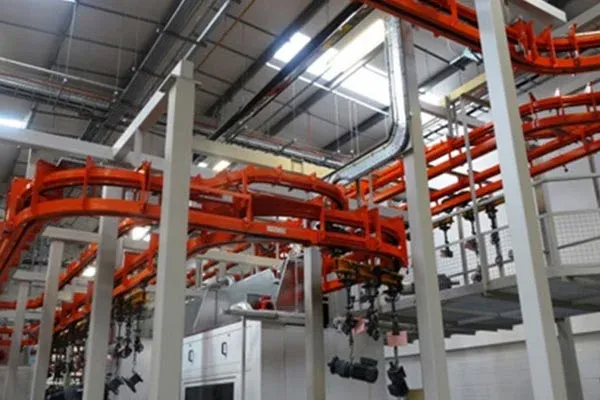
Johnston Sweepers - Overhead Conveyor
Amber Industries supplied an ATFT500 overhead conveyor system for Johnston Sweepers' paint finishing facility, designed to handle sweeper bodies weighing up to 2,000 kg with manually operated trolley movement and adjustable load bars.
Fothergill Polycom - Conveyor System
Fothergill Polycom manufactures specialist rubber compounds and coated fabrics. Explore Amber Industries' bespoke overhead conveyor solution for moving rubber between mixers and rolling mills.
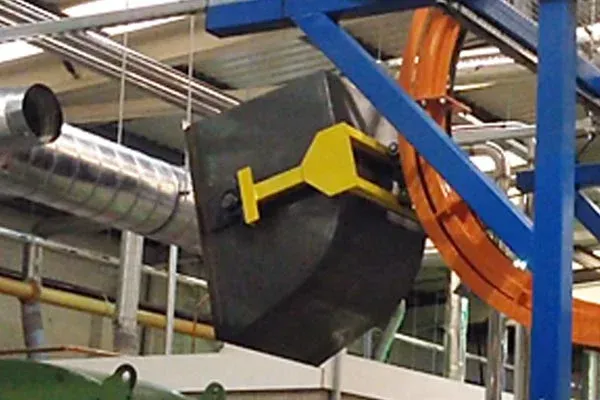
Internet Fusion - Belt Conveyor
Amber Industries supplied belt and roller conveyor systems to Internet Fusion's warehouse in Louth, Lincolnshire, transporting order-picking totes from mezzanine storage to the ground-floor packing area.
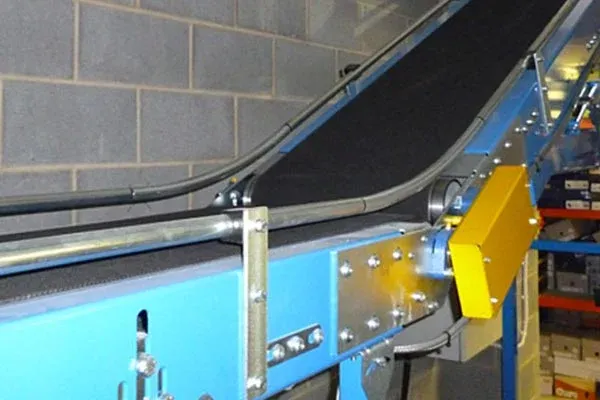
Town and Country - Dualtrack Conveyor
Town and Country Fires is a family-run stove manufacturer in North Yorkshire. Amber Industries supplied an MCM Dualtrack conveyor to streamline painting and drying operations.
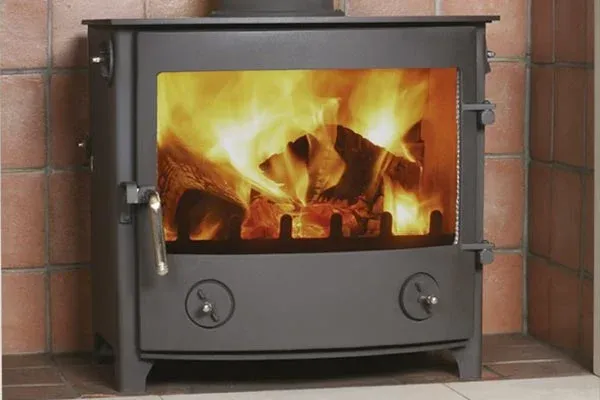
Greencroft Bottling - Roller Conveyor
See how Amber Automation integrated roller and belt conveyors into Greencroft Bottling's packaging line, improving the transfer of packed bottles to storage.
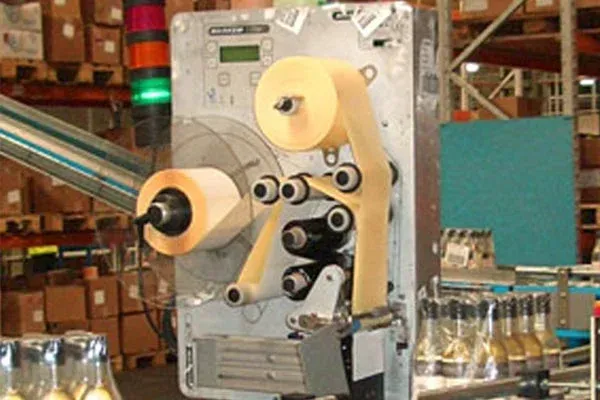
Weir Valves - Overhead Conveyor
Weir Valves & Controls needed greater flexibility and efficiency in its valve painting operations. MCM supplied an Autotrack 500 power and free overhead conveyor system to handle heavy valves through shot blasting, painting and curing.
Alliance Healthcare - Roller Conveyor
UniChem (Alliance Healthcare), a leading pharmaceutical distributor, selected Amber Industries to install a powered roller conveyor system at its Swansea delivery centre, improving order picking efficiency and tote handling.
Sandvik Paint Plant - Power & Free Overhead Conveyor
Sandvik manufactures crushing and screening equipment for the mining and quarrying industries. Amber Industries supplied an automated overhead conveyor system for its Ballygawley paint finishing plant, handling heavy components through blasting, coating and curing.