Amber Automation Pallet & Heavy Duty Chain Conveyors
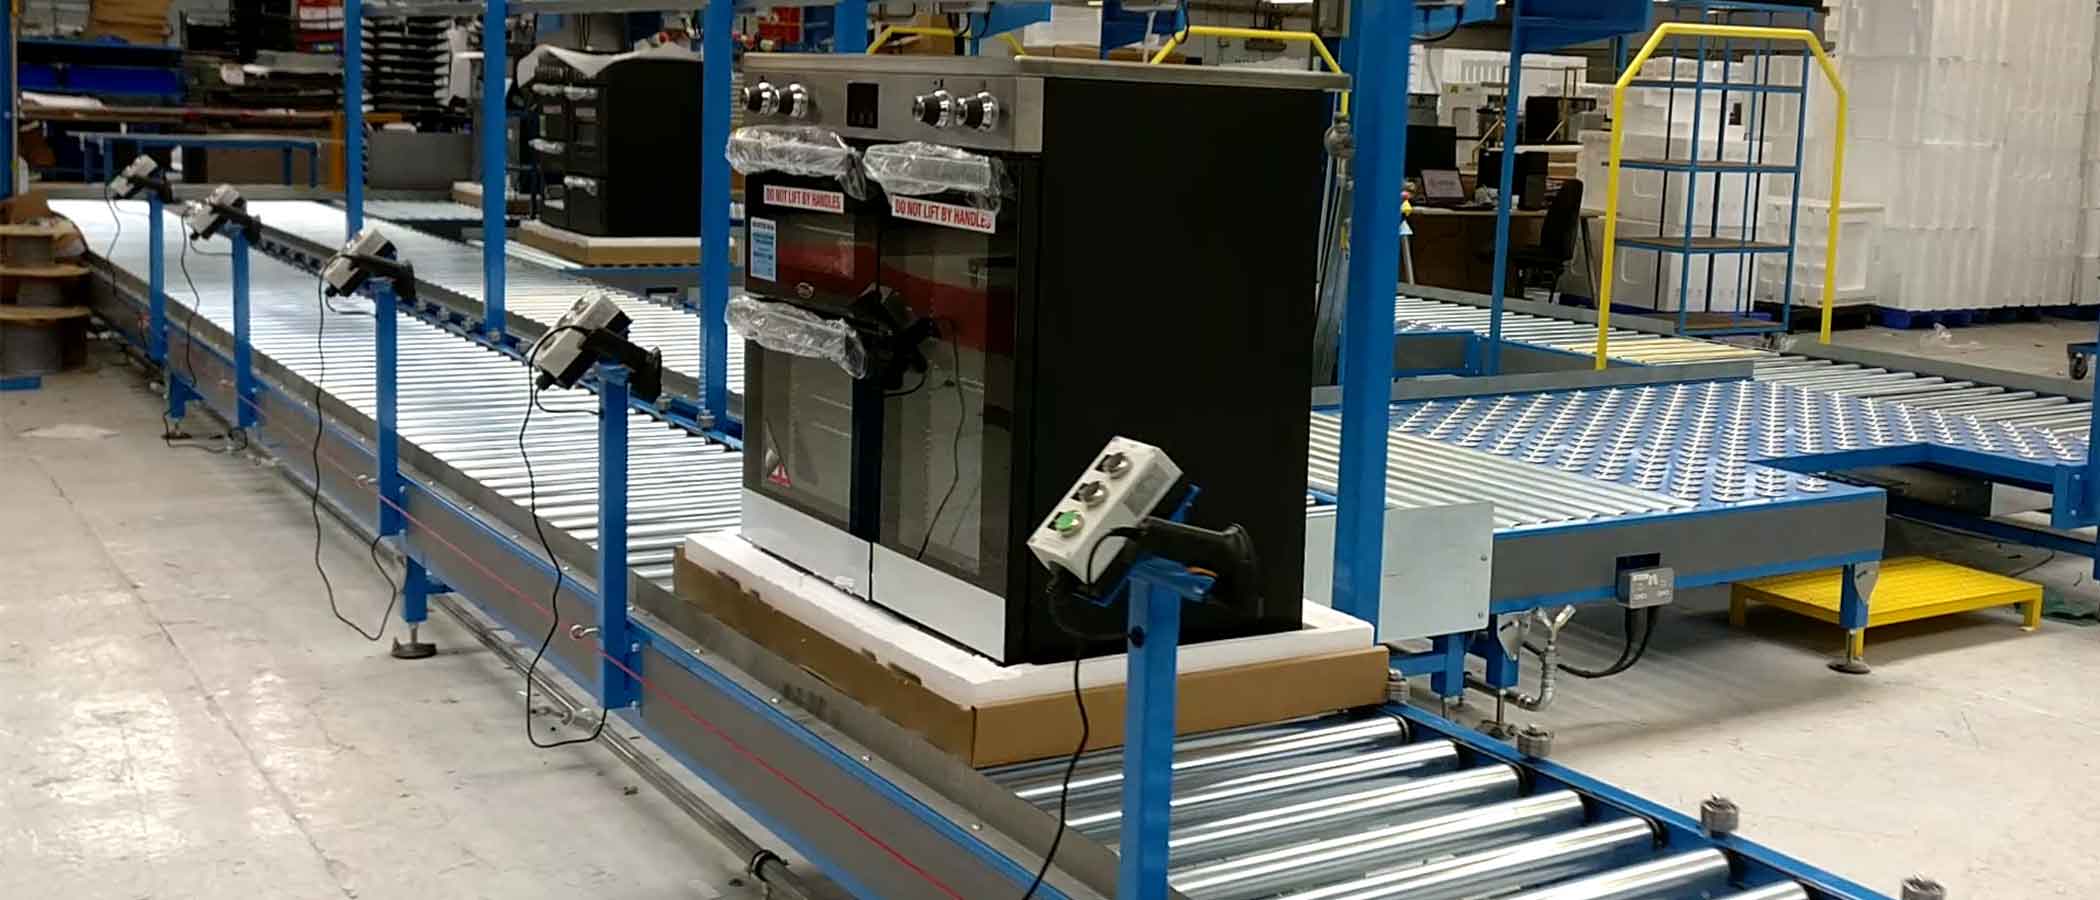
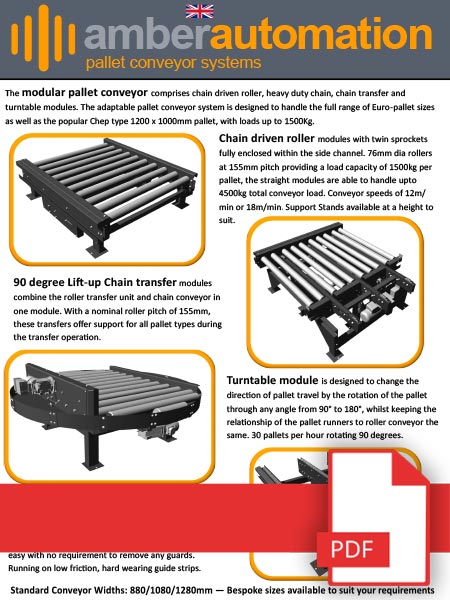
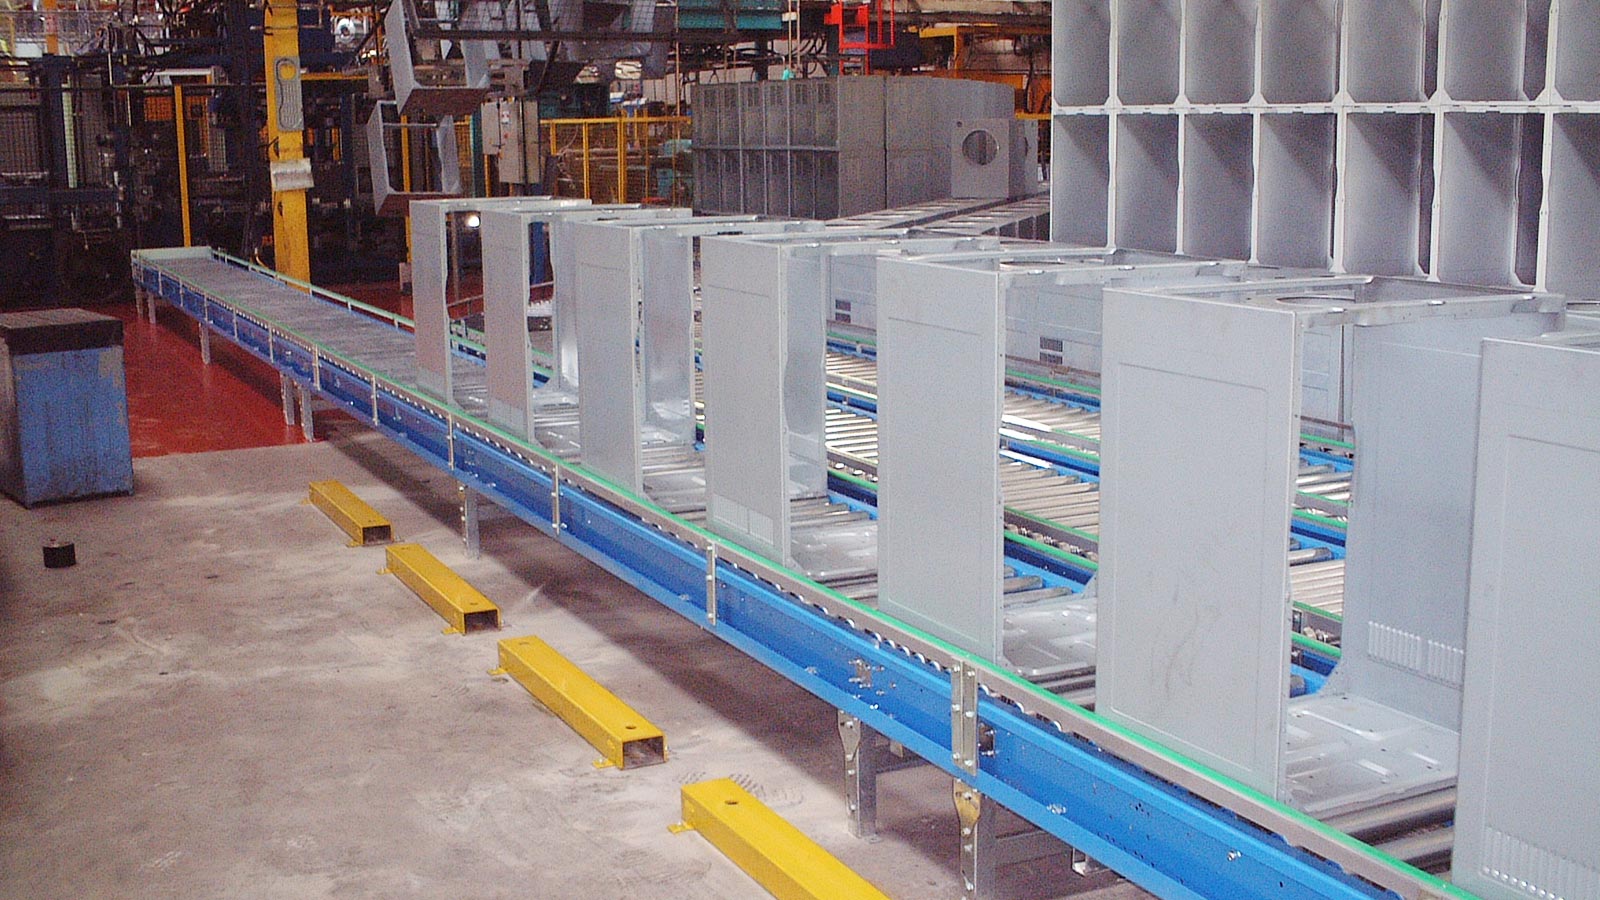
Chain driven roller conveyors are used for handling bulky and heavy products with flattish bottoms, such as loaded skids or large forgings or castings such as engine blocks etc. They are mainly used in warehouses and heavy goods lines.
Chain Drive Live Roller Conveyors
The principle of chain driven roller conveyors is that each roller is fitted with a pair of sprockets at one of its ends. The inside and outside sprockets are alternately connected to the corresponding sprocket on the adjacent rollers by a series of link chains. The terminal roller(s) are then connected via a drive chain to a geared motor incorporating an adjustable torque limiter for safety purposes. In this way a positive mechanical drive is delivered simultaneously to all of the linked rollers, ensuring that they can't slip under load. As with the lighter duty powered roller conveyors, accumulation can be built in to this type of conveyor by creating separate zones (see ZLP above) each requiring its own motor or motorised roller stop.
- Conveyor widths: various dependent on load size
- Roller diameter & pitch: typically 75mm or 90mm diameter at 125mm or 167mm
- Straight conveyor lengths: up to 6m
- Tapered rollers & turntables available
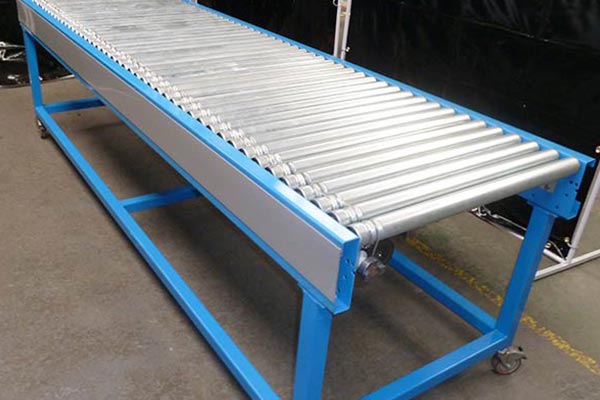
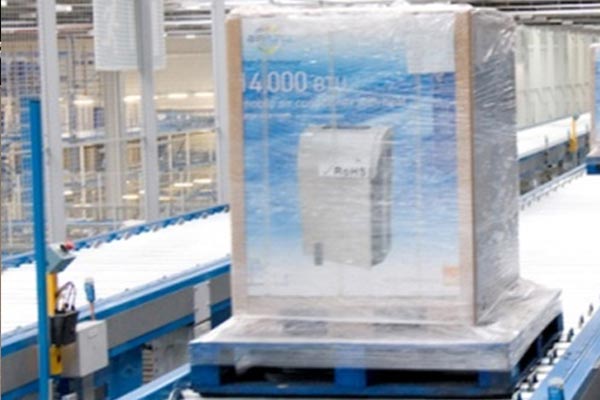
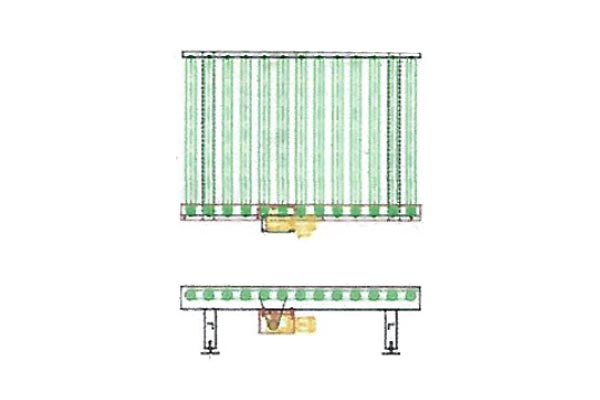
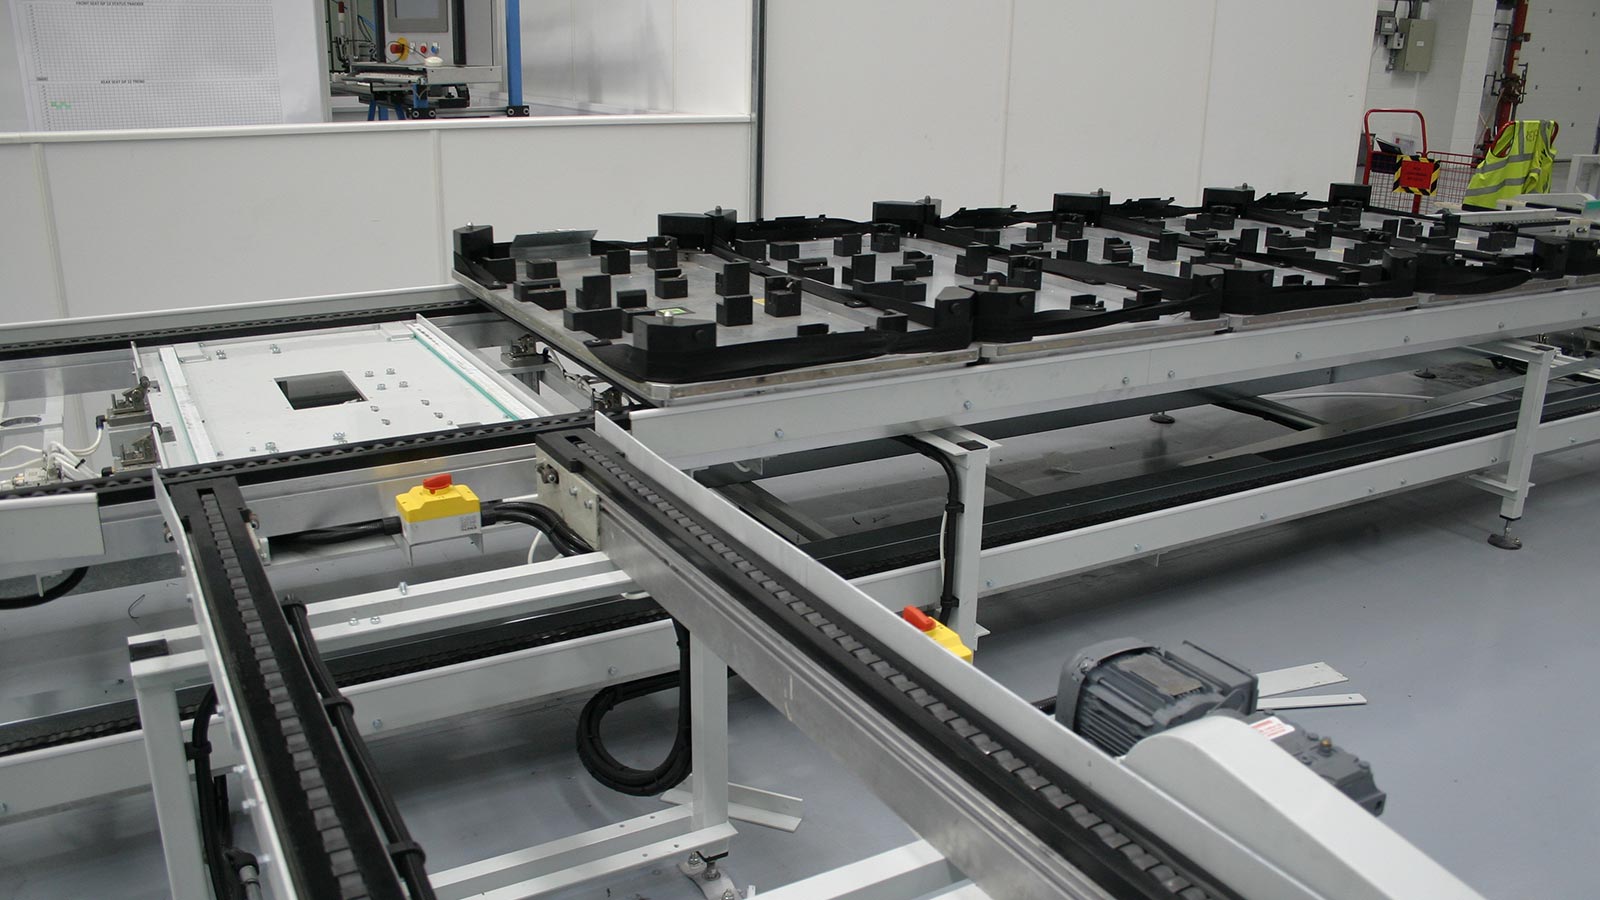
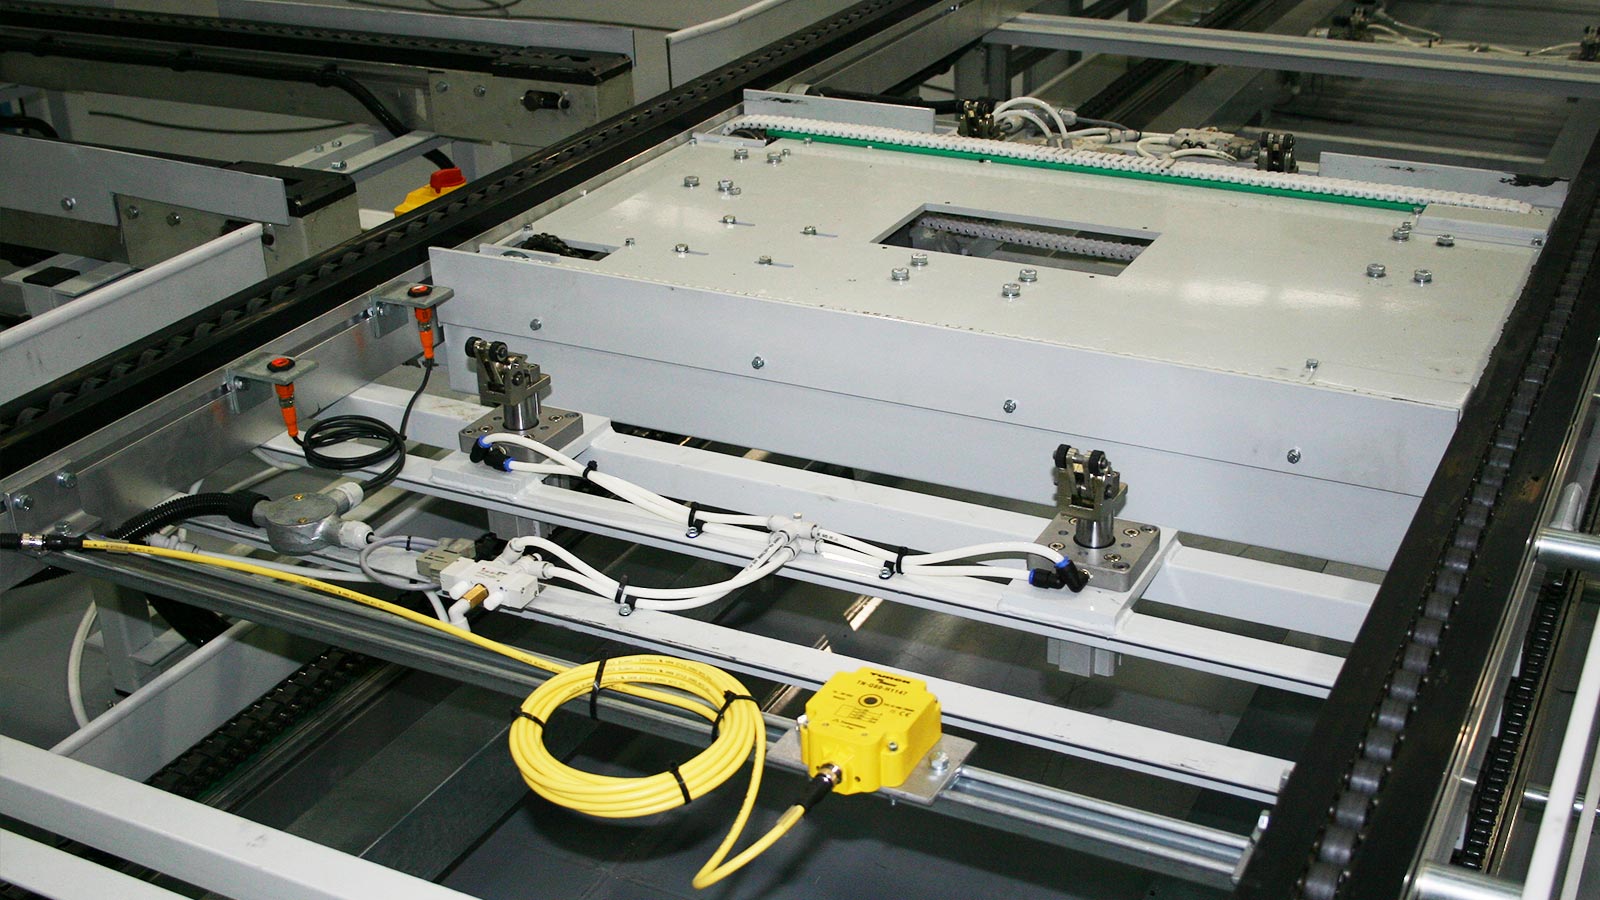
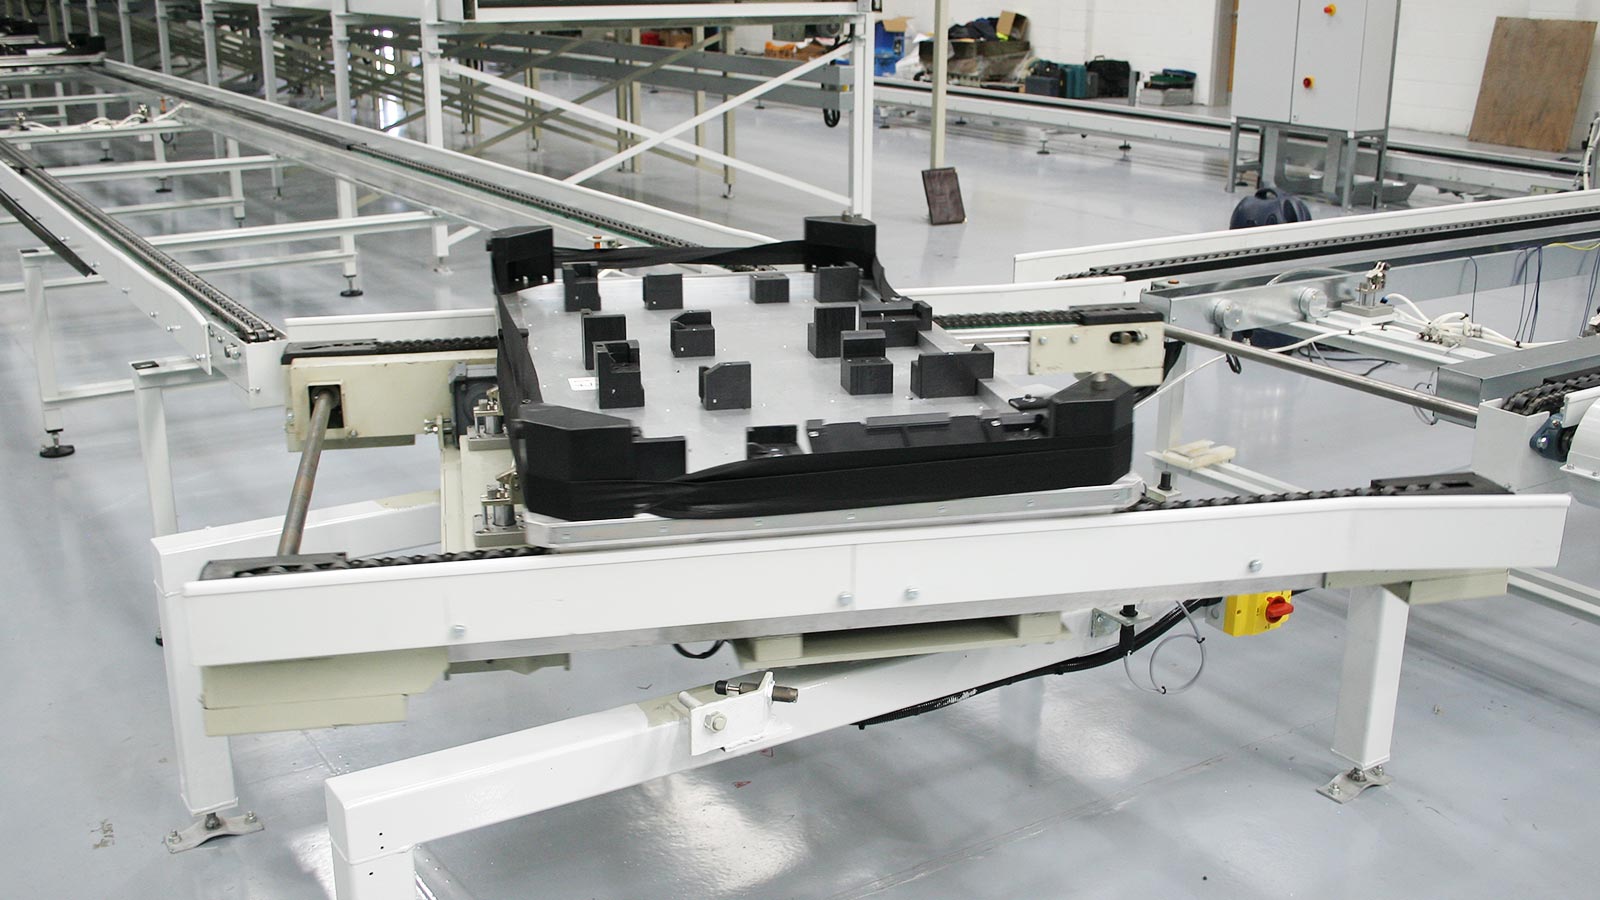
Amber Automation will design and manufacture chain drive roller conveyors with frames, widths and roller pitches and diameters specially selected for the type of load being handled. Unlike with the lighter duty powered roller conveyors the use of roller curves to change conveying direction becomes impractical as loads get heavier and so 90° transfers and turntables are used instead. Other items in the comprehensive range of ancillary equipment include shuttle cars, pallet stackers, elevators and lowerators etc.
Heavy Duty Chain Conveyors
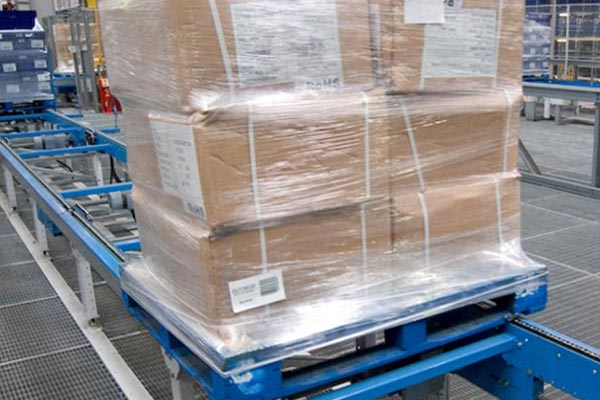
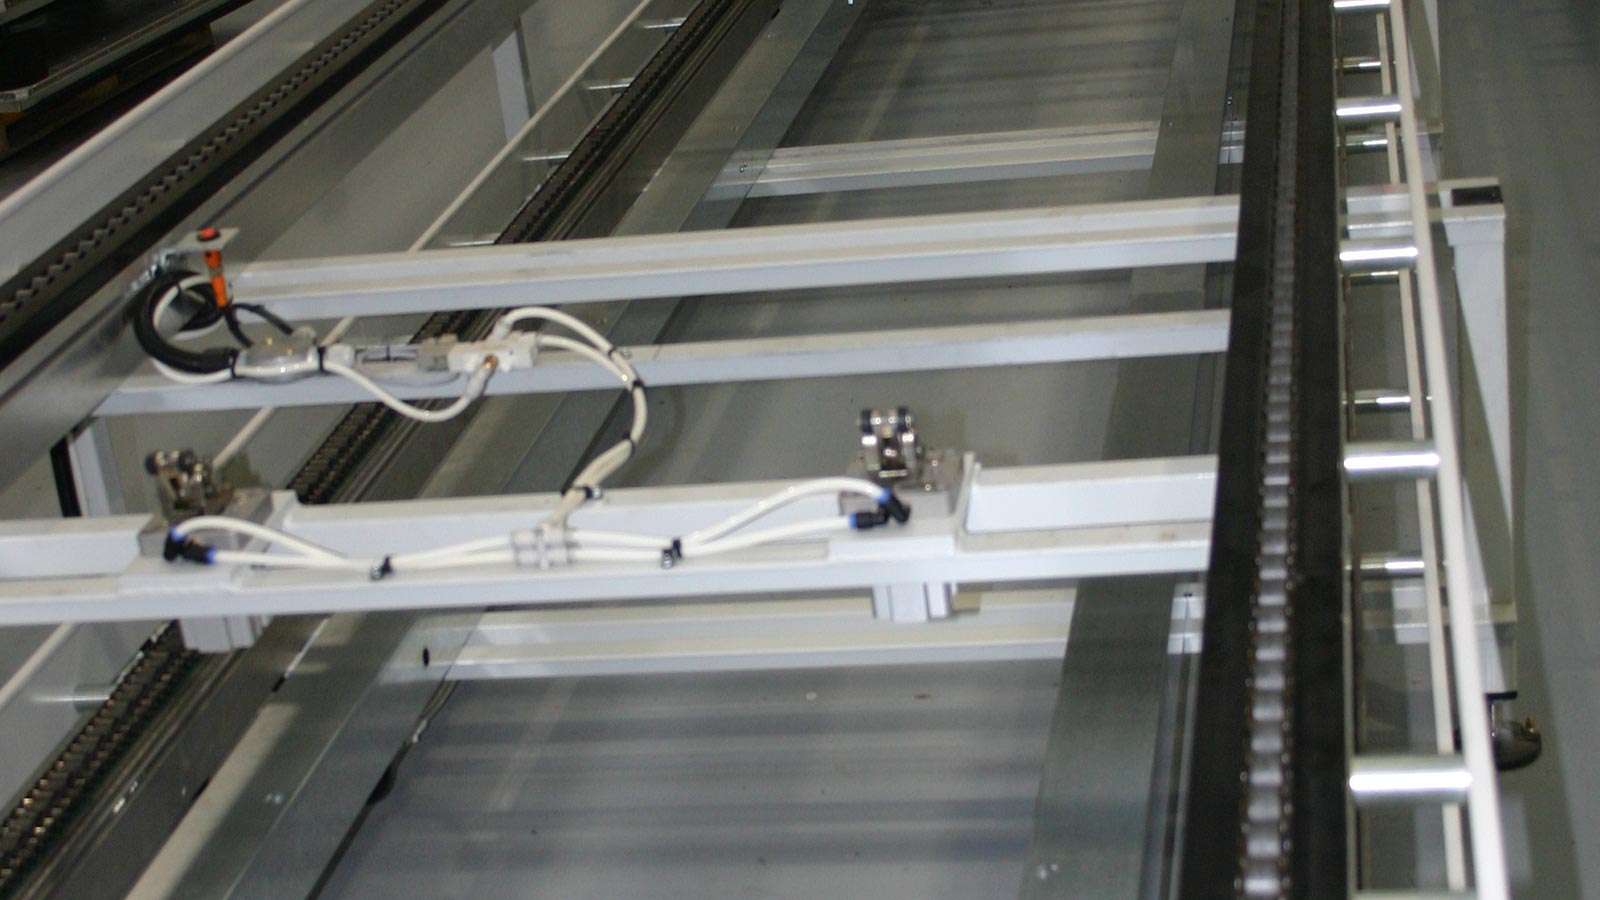
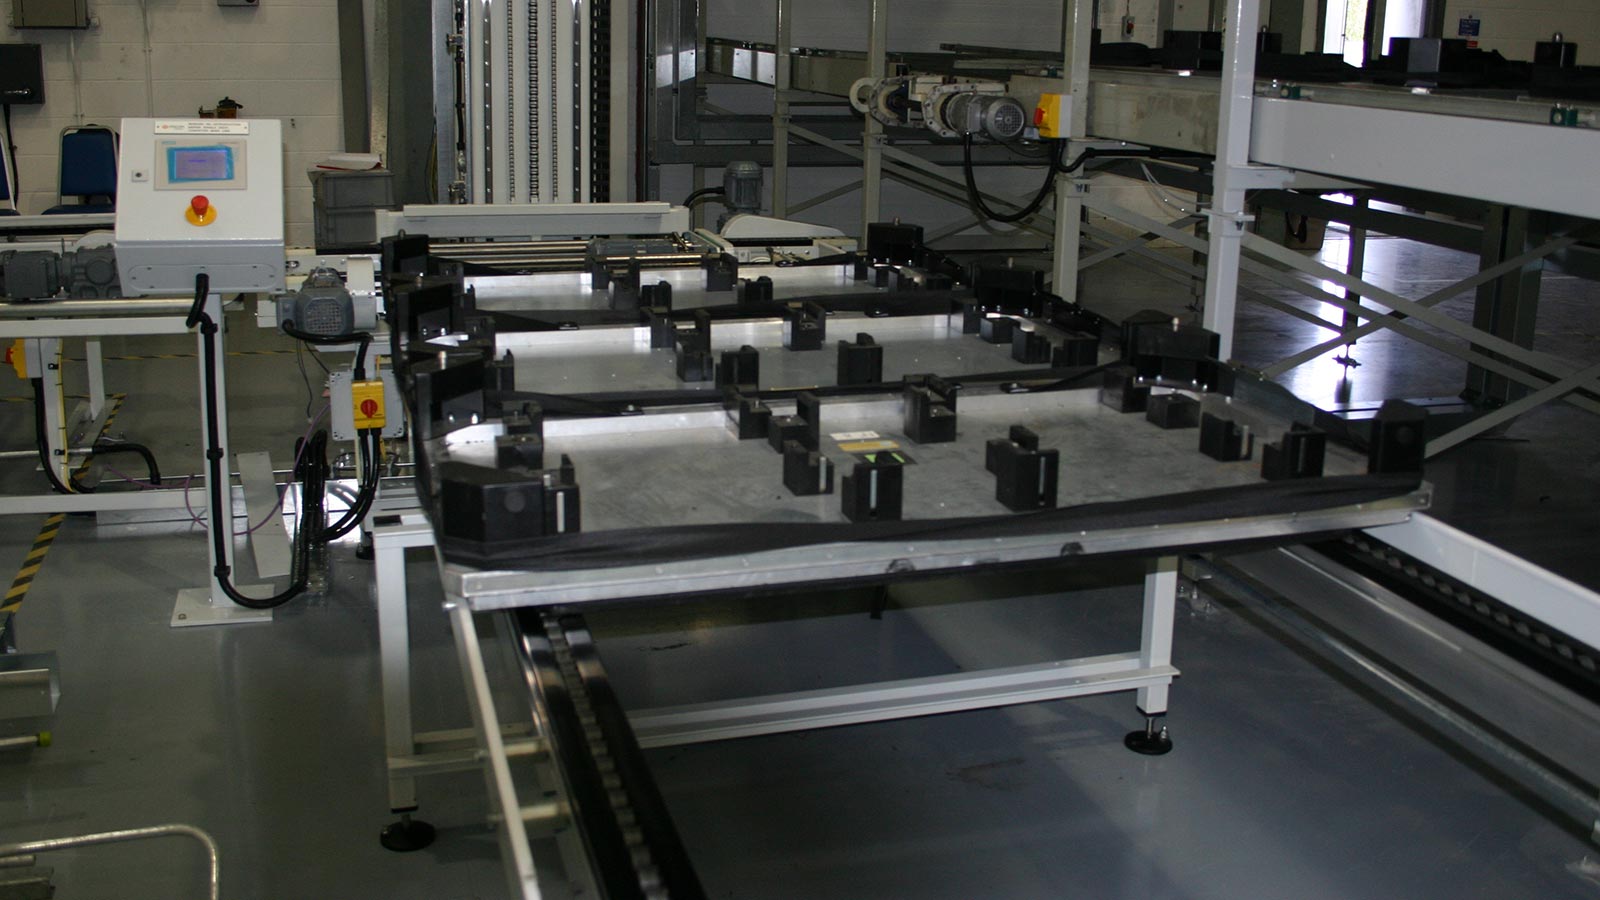
Chain conveyors are comprised of 2, 3 or multiple strands of roller bush chain guided on parallel tracks.
This type of conveyor is typically used for transporting pallets or heavy loads, nominally up to 2000 Kg, where the underside surface of the load doesn’t lend itself to running well on roller conveyors.
Cost Effective Chain Conveyors
Amber Automation's chain conveyors are a cost effective means of moving heavy loads over long distances in a straight line.
They have the added benefit of a low maintenance requirement due to few moving parts.
This characteristic, combined with their simple design and robust fabrication, makes them suitable for harsh environments, e.g. low temperatures.
Accumulation of product loads can be achieved with chain conveyors by aligning a series of short lengths, i.e. modules, each one forming a zone in the accumulation line.
Bespoke Design & Manufacture
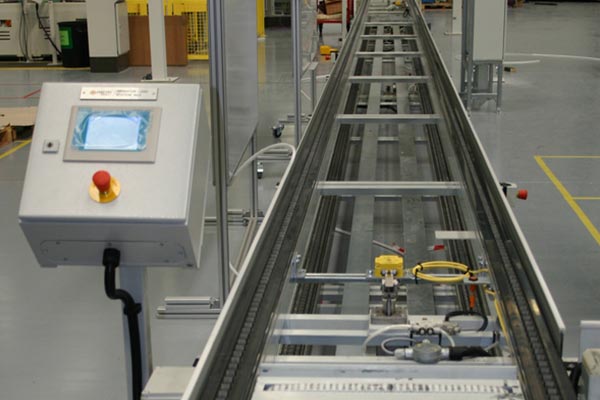
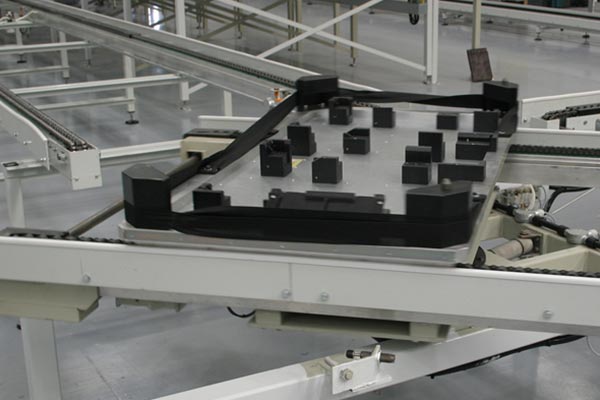
Amber Automation can design and manufacture chain conveyors in any width to suit the items to be handled and also supply all the necessary ancillary equipment to complete a turnkey chain conveyor solution, e.g. transfers, turntables, shuttle cars, pallet stackers etc.
Frequently Asked Questions About Pallet & Heavy Duty Chain Conveyors
Pallet and heavy duty chain conveyors are used for handling bulky and heavy products. Chain driven roller conveyors are suited to loads with relatively flat undersides, such as loaded skids, large forgings and castings, while heavy duty chain conveyors can transport pallets and other loads whose undersides are less suitable for roller conveyors.
Each roller is fitted with a pair of sprockets, which are connected to adjacent rollers by link chains. The terminal roller or rollers are connected by a drive chain to a geared motor, allowing a positive mechanical drive to be transmitted simultaneously to the linked rollers and helping prevent them from slipping under load.
Yes. Accumulation can be incorporated by dividing the conveyor into separate zones. Each zone requires its own motor or motorised roller stop, allowing products to be accumulated along the conveyor system.
Conveyor widths can be selected according to the size of the load. Typical roller diameters are 75 mm or 90 mm, with roller pitches of 125 mm or 167 mm, and straight conveyor sections can be supplied in lengths of up to 6 metres.
As loads become heavier, roller curves become impractical for changing conveying direction. Amber Automation therefore uses equipment such as 90-degree transfers and turntables for these applications.
A heavy duty chain conveyor consists of two, three or multiple strands of roller bush chain guided along parallel tracks. It is designed for transporting pallets and other heavy loads, particularly where the underside of the load is not well suited to travelling on roller conveyors.
Amber Automation states that its heavy duty chain conveyors are typically used for transporting pallets and heavy loads nominally up to 2,000 kg. The conveyor is designed around the requirements of the particular load and application.
Yes. Amber Automation describes its chain conveyors as having a simple design, robust fabrication and relatively few moving parts, resulting in low maintenance requirements and making them suitable for harsh environments, including low-temperature applications.
Yes. Product accumulation can be achieved by arranging a series of shorter conveyor modules, with each module forming an individual zone within the accumulation line.
Yes. Amber Automation can design and manufacture chain conveyors in widths suited to the products being handled. It can also supply ancillary equipment for a complete turnkey system, including transfers, turntables, shuttle cars and pallet stackers.