
MCM Inverted Conveyor Systems
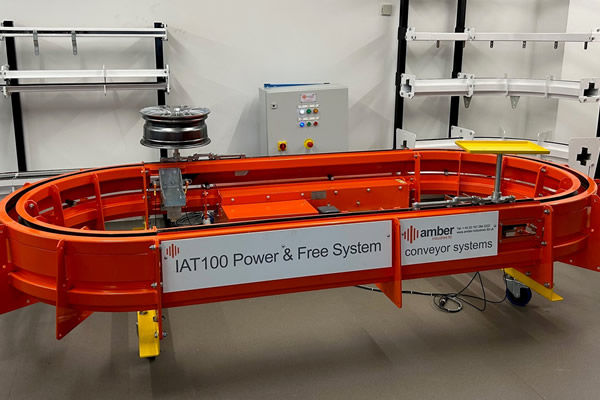
The MCM Inverted range of conveyor systems comprises the IPT100 Dualtrack. which is essentially an inverted PT100 and the IAT100 Dualtrack which is a fully functioning inverted ‘power and free’ conveyor system. Both of these conveyor systems are similar to their corresponding overhead conveyors systems except they have specifically designed features enabling them to operate in the inverted mode for carrying products at floor level.
Where a high degree of stability and precise positional accuracy is demanded an additional track (Dualtrack) is fitted on which stabilisers attached to the trolley's run.
With these inverted conveyor systems, the track and chain is below the product load being conveyed. Therefore, contaminants such as oil and other debris fall away from the product thereby eliminating a cause of potential defects and rework.




Frequently Asked Questions About MCM Dualtrack
MCM Dualtrack is a range of inverted conveyor systems designed to carry products at floor level. The conveyor track and chain run beneath the product, with a secondary stabilising rail providing the additional track that gives the Dualtrack system its name.
The MCM inverted conveyor range includes the IPT100 Dualtrack and IAT100 Dualtrack. The IPT100 is essentially an inverted PT100 conveyor, while the IAT100 is a fully functioning inverted power and free conveyor system.
MCM Dualtrack uses a powered conveyor arrangement together with a secondary stabilising rail. Stabilisers run on the additional track to provide greater stability and positional accuracy while products are transported through the conveyor system.
The system uses an additional stabilising track alongside the main conveyor track. This secondary rail supports stabilisers attached to the trolley arrangement, creating the two-track or Dualtrack configuration and providing increased product stability.
The IPT100 Dualtrack is based on an inverted PT100 conveyor, while the IAT100 Dualtrack is an inverted power and free conveyor system. The IAT100 therefore provides the additional product-flow flexibility associated with power and free conveying.
The secondary stabilising rail provides additional support to the product-carrying arrangement, giving the conveyor a high degree of stability. This makes MCM Dualtrack particularly suitable for applications where repeatable and precise positioning of the product is required.
Because the conveyor track and chain are positioned beneath the product, contaminants such as lubricating oil and other debris fall away from the conveyed item rather than onto it. This helps reduce a potential source of product defects and rework.
Yes. The combination of stable product handling, accurate positioning and an inverted conveyor arrangement makes MCM Dualtrack suitable for manufacturing, finishing, inspection and automated handling applications where product stability and cleanliness are important.
Yes. Dualtrack systems can be engineered for applications requiring product rotation. Amber Industries has supplied a Dualtrack system for a stove manufacturing paint process where products needed to rotate in front of an operator during paint application while remaining stable on the conveyor.
MCM Dualtrack combines floor-level product handling with high stability and accurate positioning. Its inverted arrangement also allows oil and debris to fall away from the product, while the IAT100 version provides the additional flexibility of an inverted power and free conveyor system.