


Amber Industries - UK Conveyor Systems & Material Handling Solutions
Amber Industries is a UK-based designer and manufacturer of conveyor systems and material handling solutions, with a heritage spanning more than 60 years. We supply everything from individual belt conveyors and roller conveyors to fully integrated automated conveyor systems, helping businesses improve efficiency and productivity across manufacturing, processing, warehousing and distribution operations.
Our extensive conveyor range includes overhead conveyor systems, power and free conveyors, inverted chain conveyors, floor conveyor systems, pallet handling conveyors and powered belt curves. We also design and manufacture bespoke material handling systems tailored to individual production requirements, from straightforward conveying applications to complex integrated automation projects.
Our conveyors are manufactured in the UK to rigorous quality standards and designed around each customer's specific requirements using modern 3D CAD software. Our in-house engineers develop conveyor control systems, including PLC programming and automation software, while our experienced site technicians undertake installation and commissioning. This integrated approach enables Amber Industries to provide comprehensive conveyor solutions, from initial design and manufacture through to installation and ongoing technical support.



Overhead Conveyor Systems
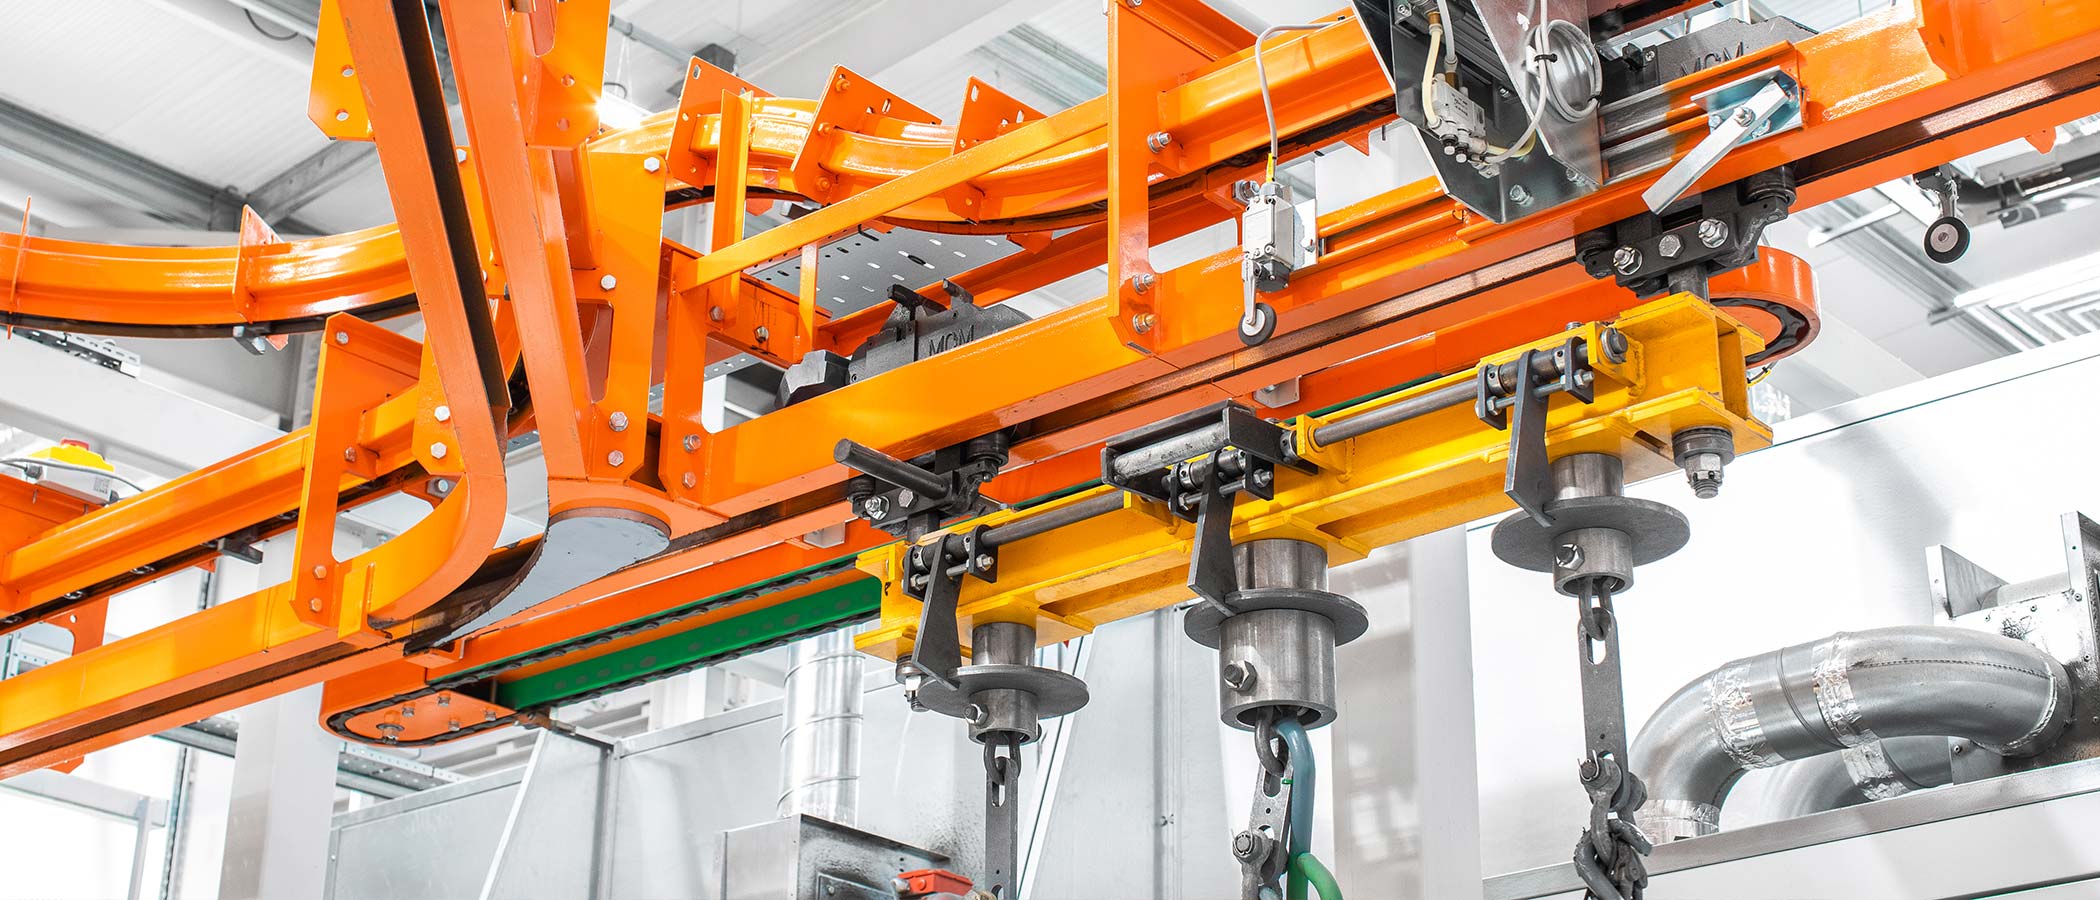
Amber Industries' MCM overhead conveyor systems have been used in industrial and manufacturing environments for over 40 years, helping businesses improve material handling efficiency, production flow and the use of available factory space. By transporting products above floor level, overhead conveyors can free up valuable working areas while providing a flexible solution for moving components between processes.
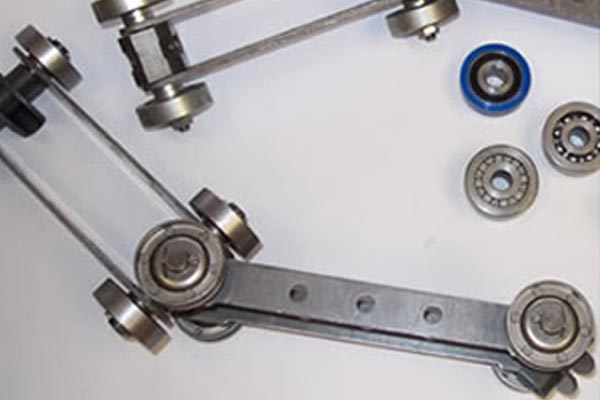
Our extensive MCM range includes Powertrack powered monorail conveyors, Autotrack power and free conveyors, Sidetrack monorail systems, Dualtrack inverted conveyors and Freetrack manually operated trolley systems. Each range offers different handling capabilities, allowing us to develop conveyor layouts suited to specific products, processes and production requirements.
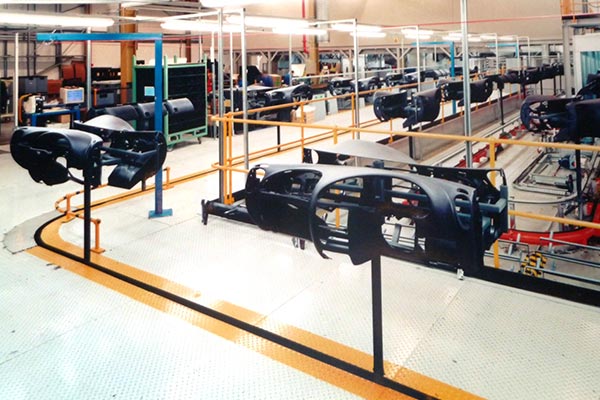
Our overhead conveyors are used for assembly lines, component transportation, product storage and distribution, as well as surface finishing processes including shotblasting, cleaning, degreasing, painting, powder coating, plating and oven curing. Applications span automotive manufacturing, commercial vehicles, agricultural machinery, industrial equipment, food processing and consumer goods production.
Floor Conveyor Systems
Amber Automation, a specialist division of Amber Industries, designs and manufactures floor conveyor systems for the efficient movement of products and materials within manufacturing, warehousing and distribution environments. From simple manually operated conveyors to fully integrated automated handling systems, our solutions are designed to improve material flow, reduce manual handling and make effective use of available space.
Our extensive range includes powered and gravity roller conveyors, level and incline belt conveyors, heavy-duty chain conveyors and pallet conveyor systems. We also supply steel slat, modular plastic and wire mesh belt conveyors, laundry conveyors and a wide range of ancillary conveyor equipment, including transfers, turntables, personnel gates and shuttle cars.
Floor conveyor systems are widely used for transporting cartons, totes, cases, pallets and other unit loads. Applications include warehouse and distribution operations, e-commerce fulfilment, parcel handling, packaging, food and beverage production, automotive manufacturing and industrial assembly lines. Conveyor layouts can incorporate accumulation, sorting, transfers and changes in elevation to accommodate different handling requirements.
Whether the requirement is for an individual conveyor or a complex automated material handling installation, Amber Automation's experienced mechanical and control systems engineers can develop a solution tailored to the application. Combining UK-manufactured conveyor equipment with suitable specialist components where required, we provide integrated systems designed around each customer's operational needs.
Spares & Services
Amber Industries provides conveyor spare parts, maintenance and repair services to help customers maintain reliable operation and minimise unplanned downtime. Our experienced service engineers support conveyor systems throughout their working life, from routine maintenance to repairs, modifications and refurbishment.
Our services include planned preventative maintenance, breakdown call-outs, conveyor chain replacement, condition surveys, system refurbishment, conveyor extensions and on-site training. We work with customers to maintain the performance and reliability of their material handling equipment and help adapt existing installations to changing production requirements.
Bespoke Handling Solutions
Amber Industries designs and manufactures bespoke material handling equipment for applications where standard conveyor systems alone cannot meet specific operational requirements. Our experienced engineering team develops specialist solutions for lifting, transferring, sorting, turning and storing products, with equipment designed around individual production processes, product characteristics and site layouts.
Our bespoke handling projects include an automatic beam unloader for transferring painted components, cooling and storage units for manufactured products, turnover units for handling delicate materials and package sorting systems. We also provide specialist laundry conveyor systems, food processing conveyor lines and lifting elevator units for transferring loads between different floor levels.
Whether developing a standalone handling machine or integrating specialist equipment into a larger automated conveyor system, Amber Industries combines mechanical design, manufacturing and control systems expertise to deliver solutions tailored to each customer's requirements. Our bespoke approach enables us to address unusual handling challenges, improve production efficiency and make effective use of available space.
Powered Belt Curves
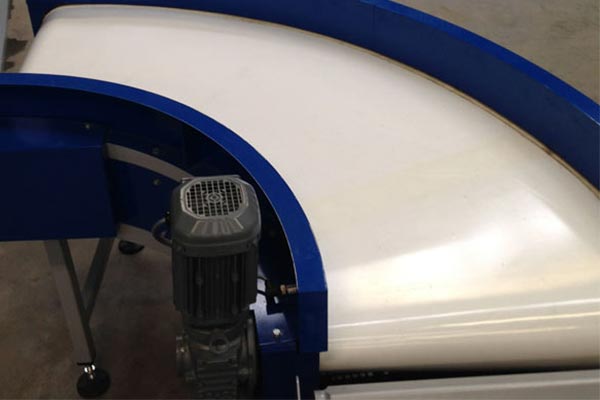
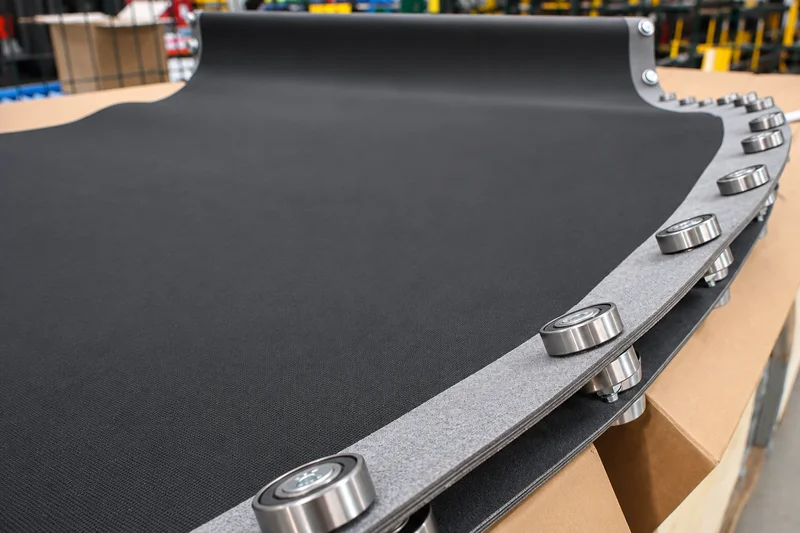
Amber Industries manufactures Gramac Quartz powered belt curves, specialist curved belt conveyors designed to change the direction of conveyed products smoothly and efficiently while maintaining their orientation. Also known as belt bends, belt turns or power bends, these conveyor systems are widely used in industrial manufacturing, warehousing, distribution and airport baggage handling applications.
With over 30 years of experience in belt curve manufacturing, Gramac Quartz offers a comprehensive range of UK-manufactured conveyors in different curve angles, belt widths and load capacities. Standard configurations are available alongside bespoke designs developed to meet specific layout and operational requirements. Our belt curves are engineered for reliable operation, long service life and low maintenance, even in demanding industrial environments.
Our powered belt curves are used in warehousing, distribution and intralogistics, manufacturing and processing industries, and airport baggage handling systems. For more demanding applications, our TR200 heavy-duty belt curves offer a load capacity of up to 200 kg/m, with options for thicker, abrasion-resistant or cut-resistant belts.
Discover the design advantages and features of Gramac Quartz belt curves, or view our technical data and specifications for dimensions, performance information and CAD drawings.
Conveyor Systems Case Studies
Amber Industries has designed, manufactured and installed conveyor systems for customers across a wide range of manufacturing, processing, warehousing and distribution industries. Our projects demonstrate how overhead conveyor systems, floor conveyors and bespoke material handling solutions can be tailored to meet specific operational requirements, improve production efficiency and streamline material flow.
Our experience includes conveyor installations for organisations such as SEW Eurodrive, Johnston Sweepers, Sandvik, Greencroft Bottling and Alliance Healthcare. From automated overhead conveyors for paint finishing facilities to roller and belt conveyor systems for packaging and order picking operations, our case studies provide practical examples of the engineering solutions delivered by Amber Industries.
Discuss Your Conveyor System Requirements
Looking for a conveyor system for your manufacturing, processing or distribution operation? From individual conveyors to fully integrated material handling systems, our experienced engineering team can help develop a solution suited to your requirements.
Latest News
10th November 2026
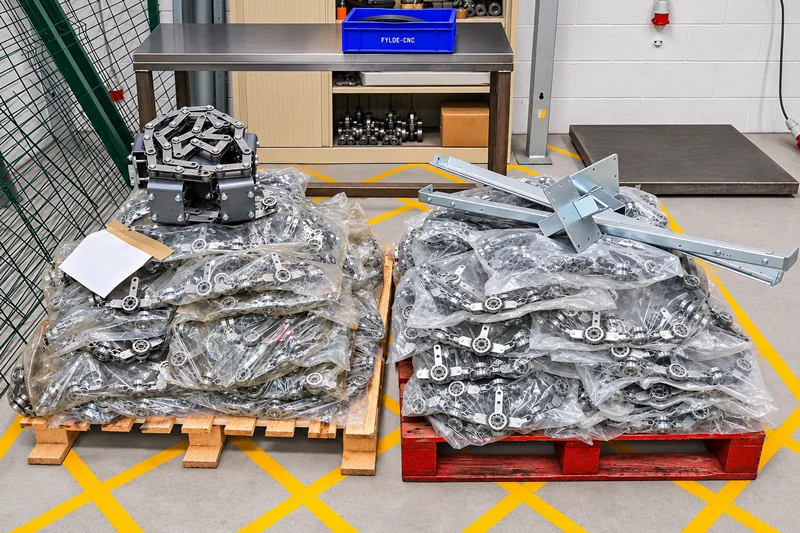
Amber Industries Supplies MCM Powertrack PT60 Conveyor Chain To Electrical Infrastructure Manufacturer In Ireland
READ MORE >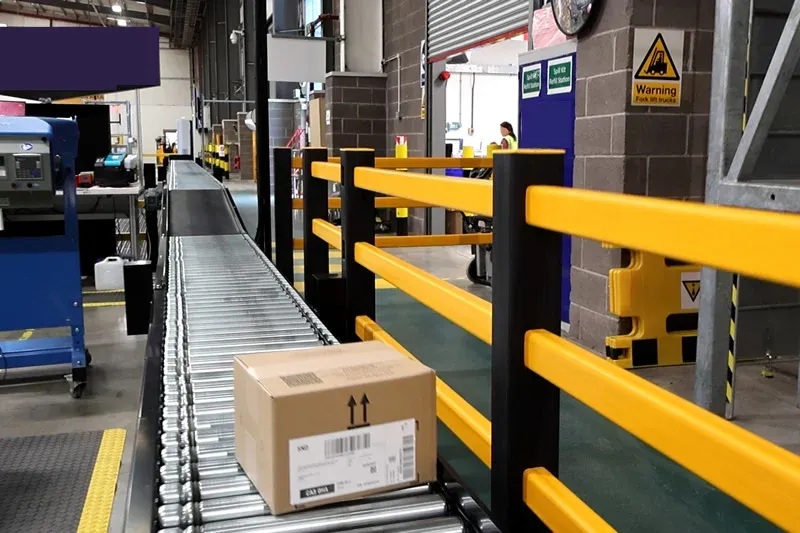
30th October 2026
New Lineshaft Conveyor System Enhances Distribution Operations For Global Beauty Product Organisation
READ MORE >