Who We Are
Amber Industries Ltd is a leading UK designer, manufacturer and supplier of conveyor equipment and systems, with over 40 years' experience in the automated mechanical handling and conveyor industry.
For many of our clients, the safe, timely and cost-effective movement of goods through their facilities is critical to their operations. Our mission is to improve operational efficiency by providing innovative, expertly tailored conveyor solutions at competitive prices.
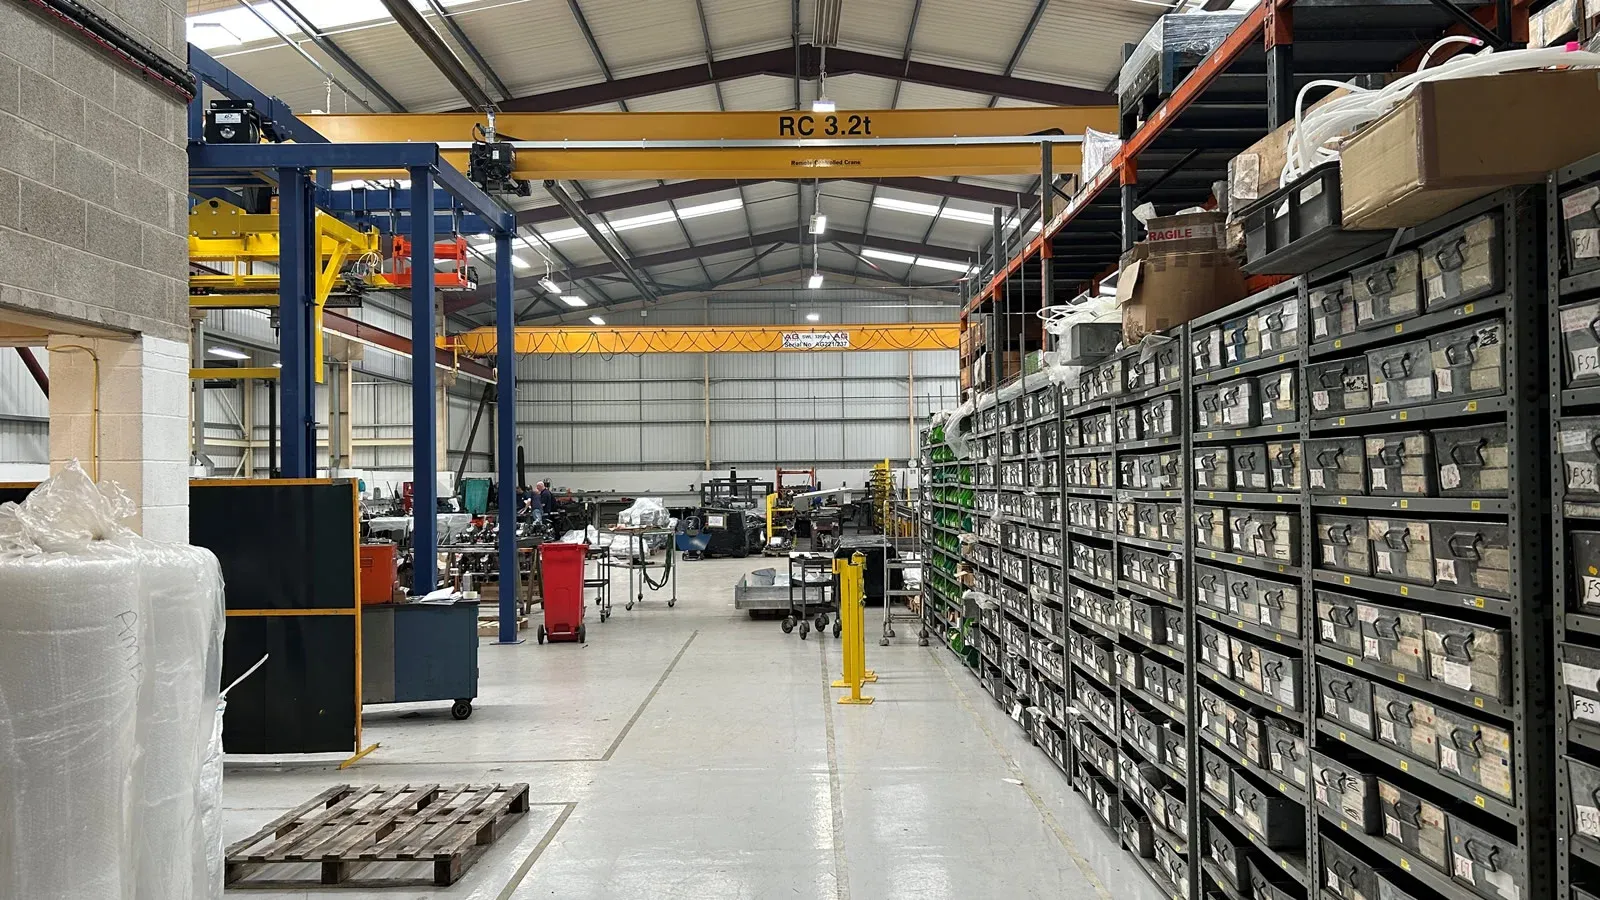
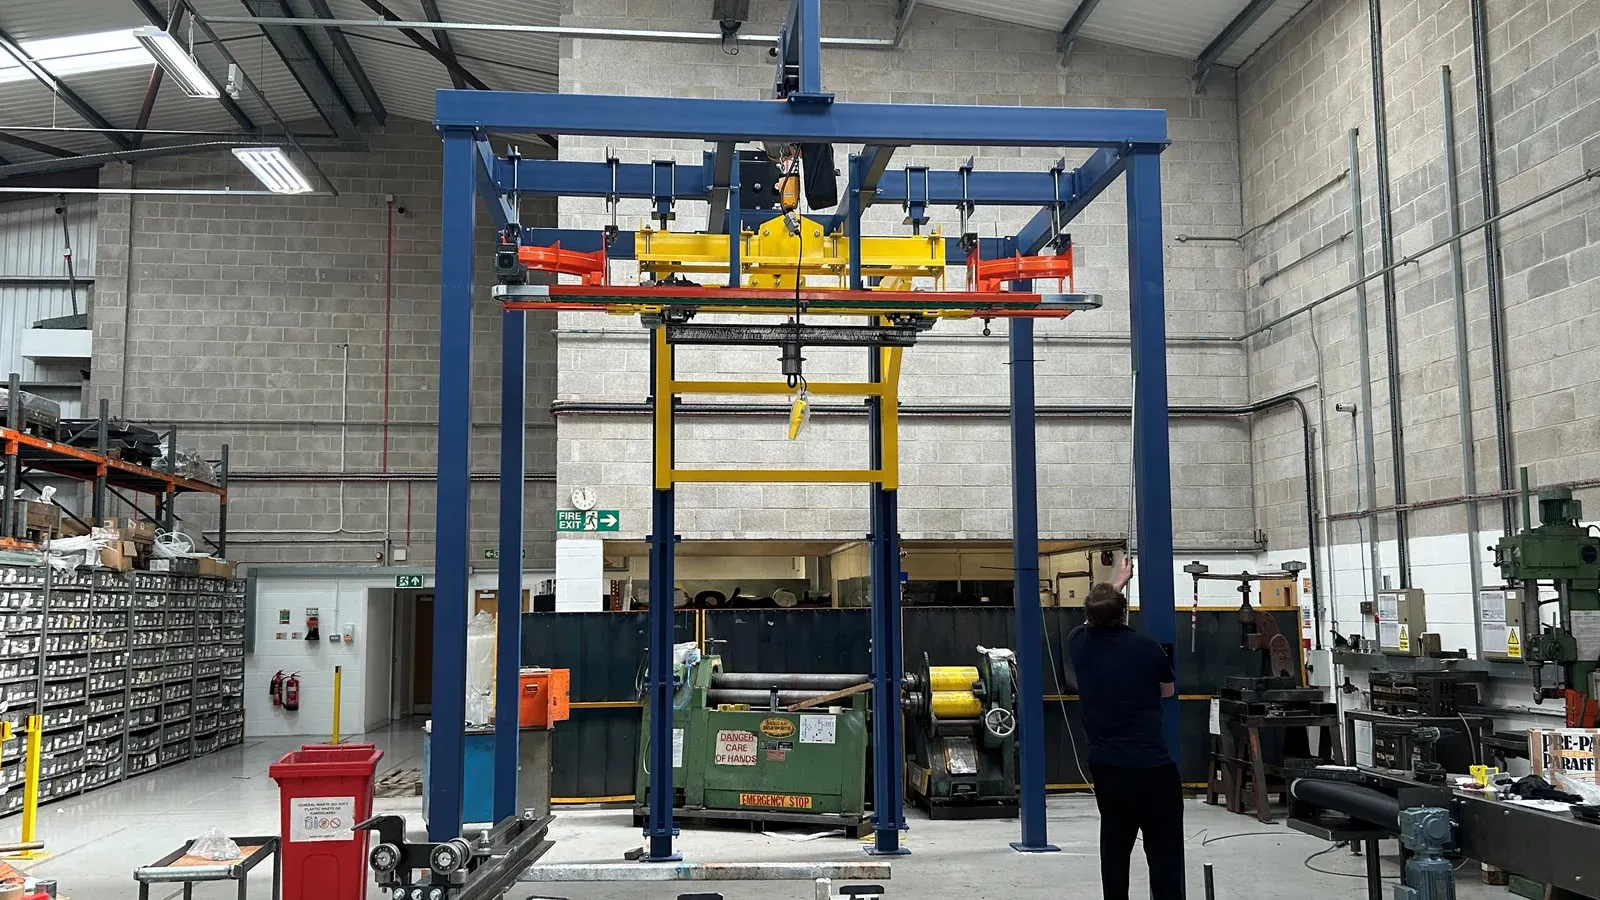
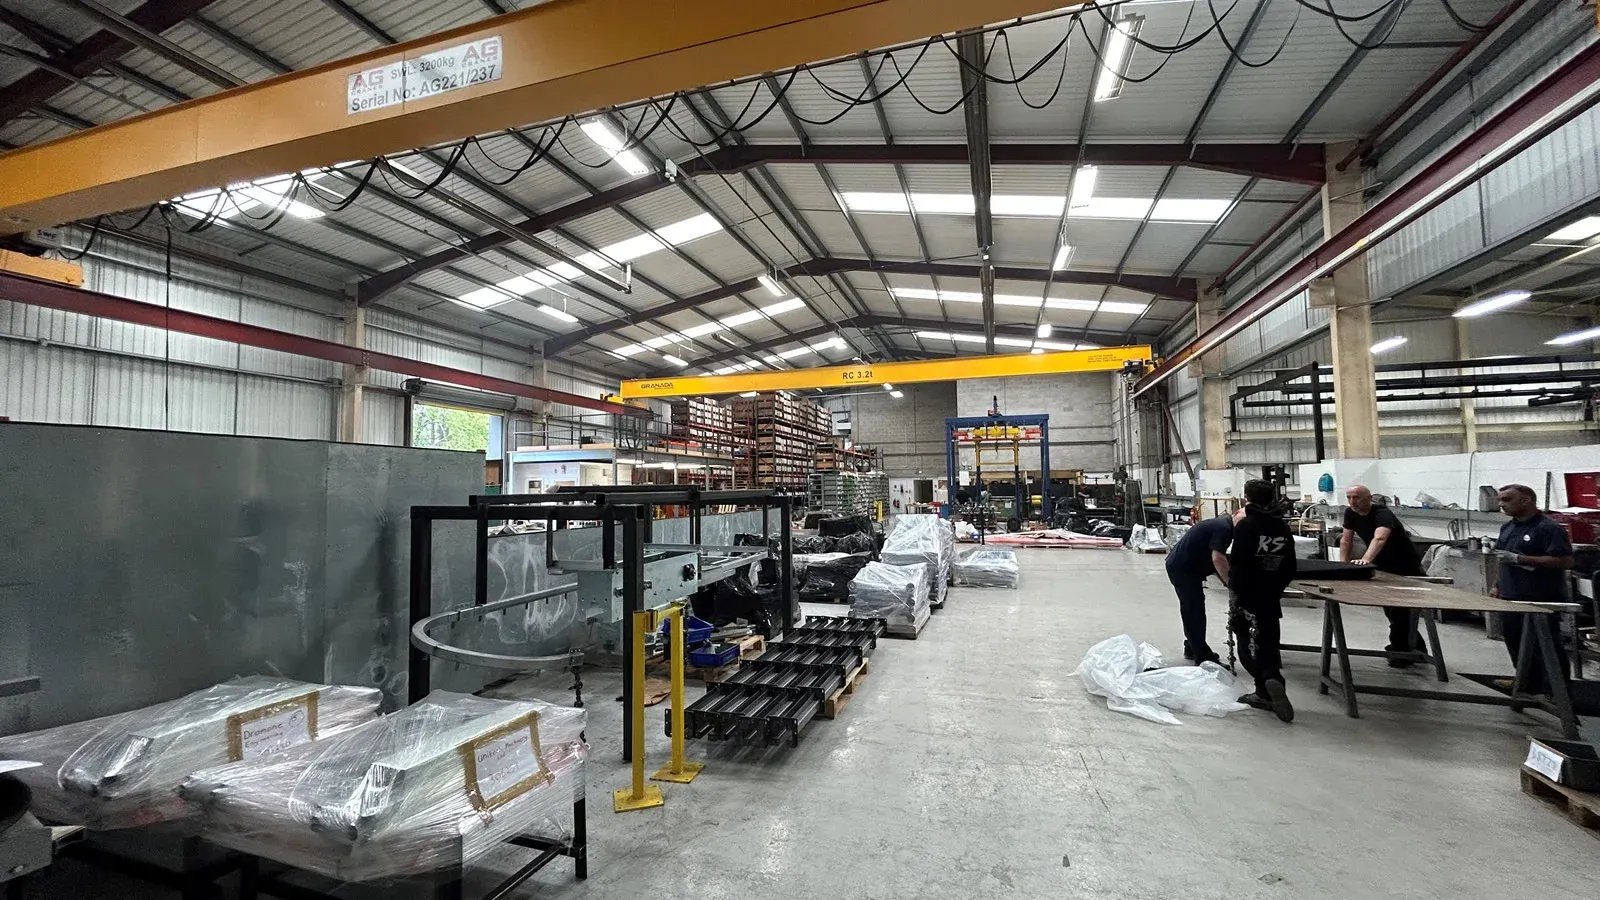
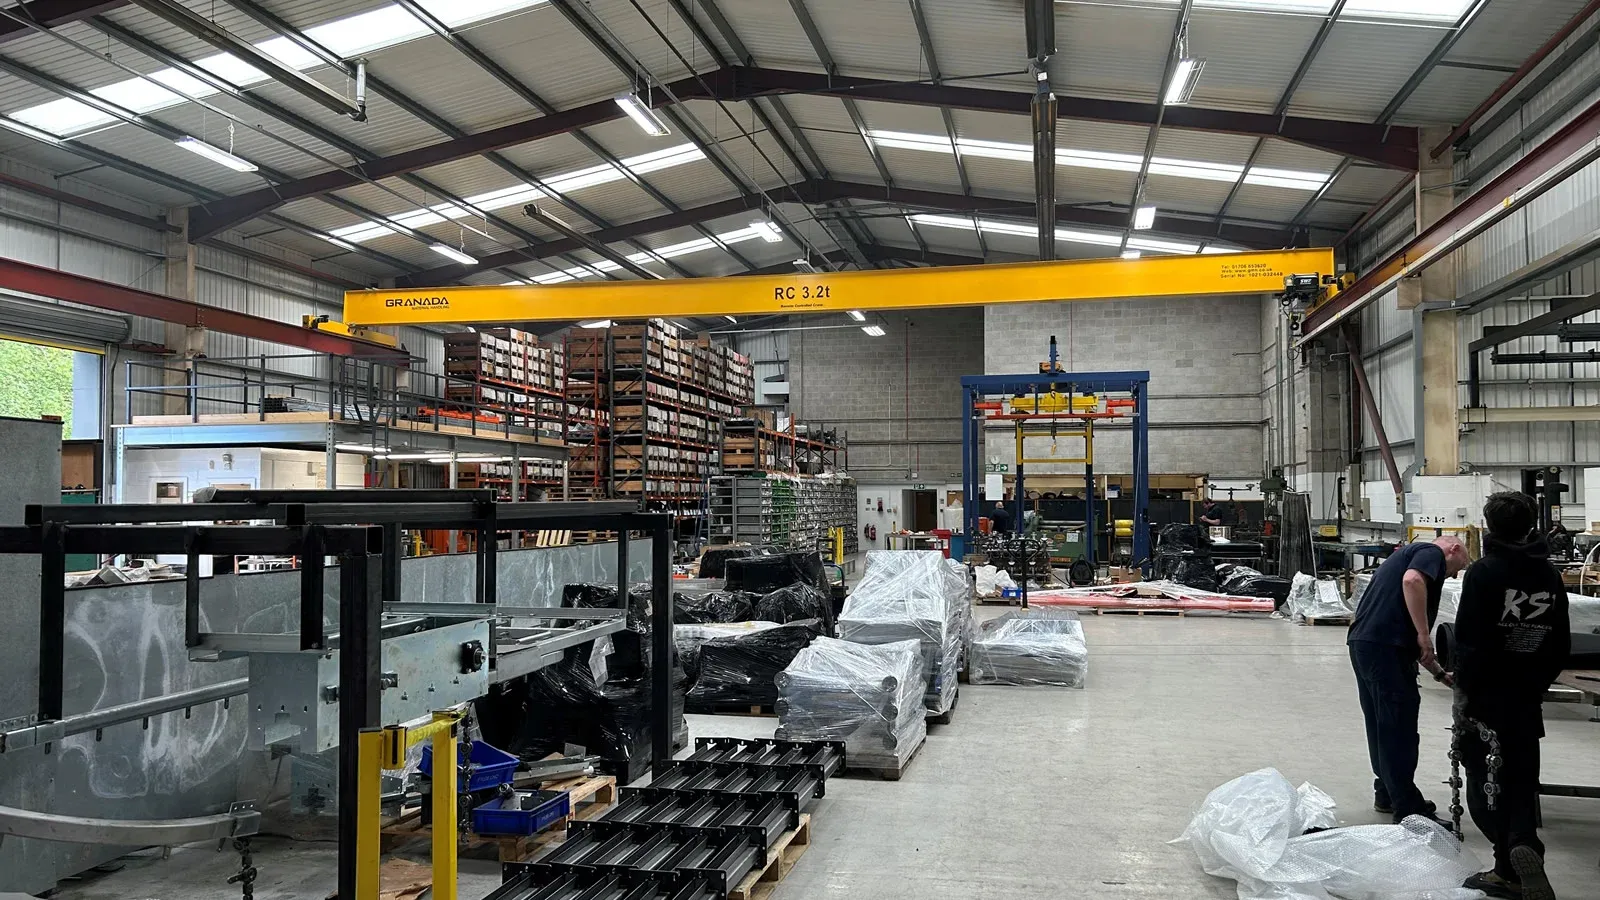
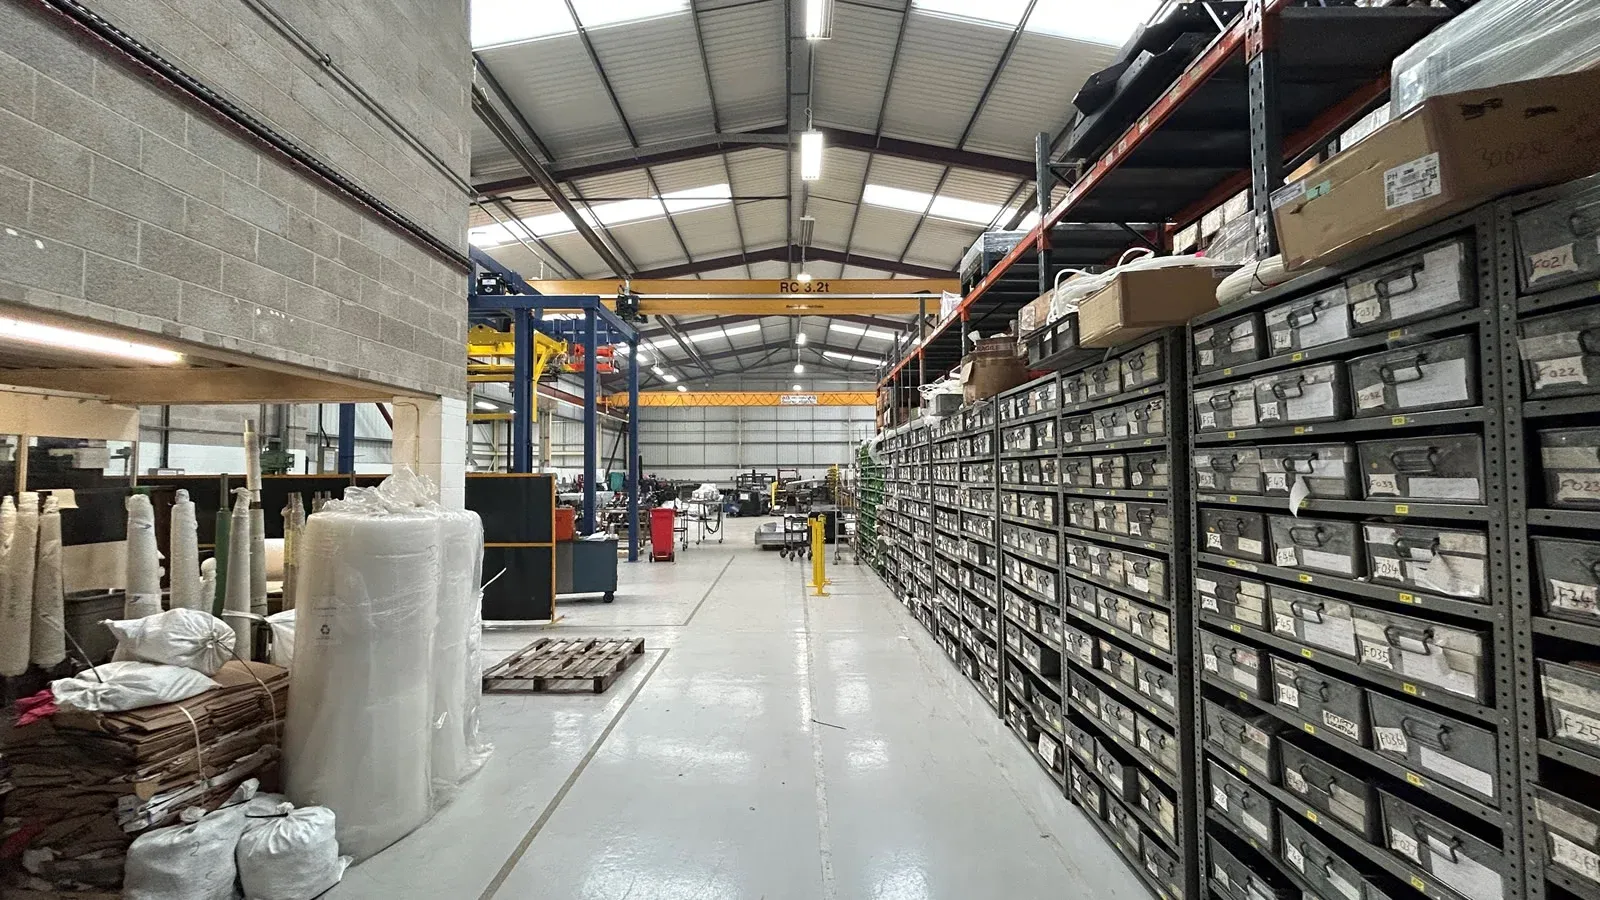
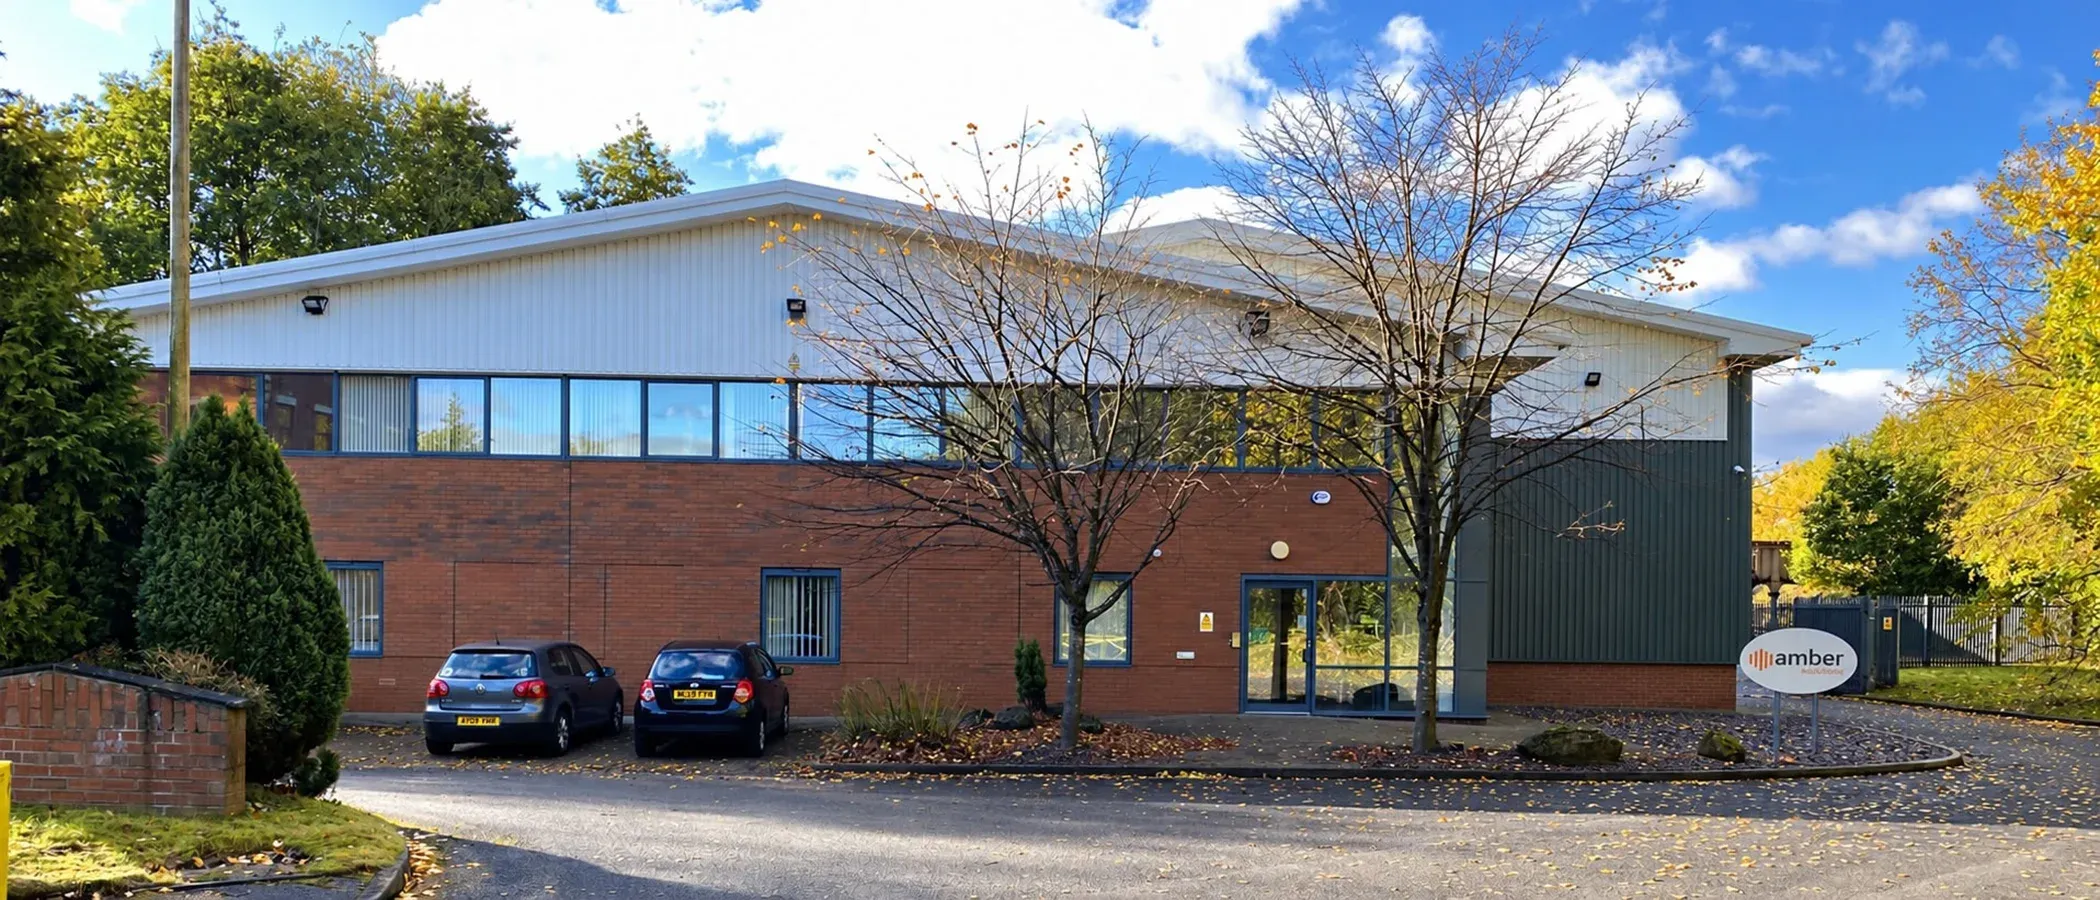
Amber Industries operates from a 2,000-square-metre manufacturing facility in Oldham, Greater Manchester, UK. The facility houses our engineering, production and assembly operations, together with an extensive stock of conveyor components and spare parts.
Our strength lies in our in-house teams of specialists, whose combined expertise enables us to design, manufacture and install bespoke conveyor equipment and complex automated conveying systems. These teams include mechanical design engineers, control systems engineers, manufacturing engineers, installation and commissioning engineers, and service technicians who provide ongoing maintenance and support for our systems and products.
Latest Technology
Amber Industries regularly invests in technology to support efficient engineering, manufacturing and business operations. Our comprehensive Enterprise Resource Planning (ERP) system integrates core business processes, while 2D and 3D computer-aided design (CAD) software and project management tools support our engineering teams throughout the design and delivery of conveyor systems.
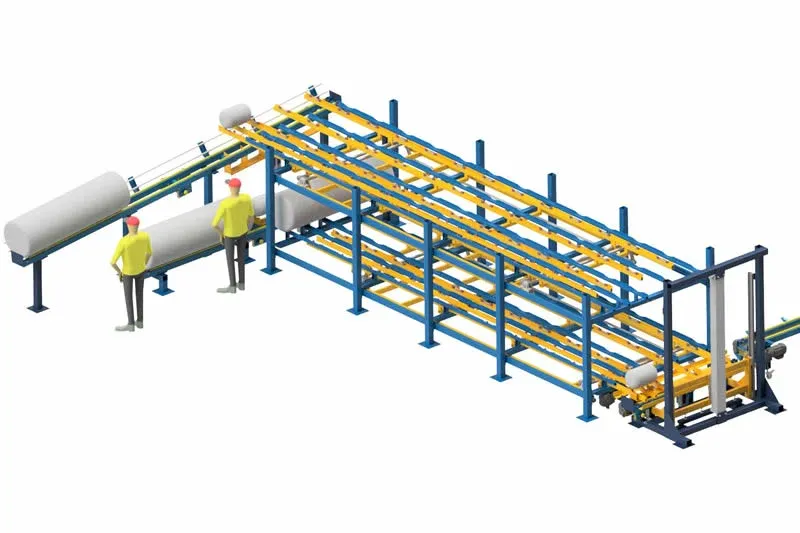
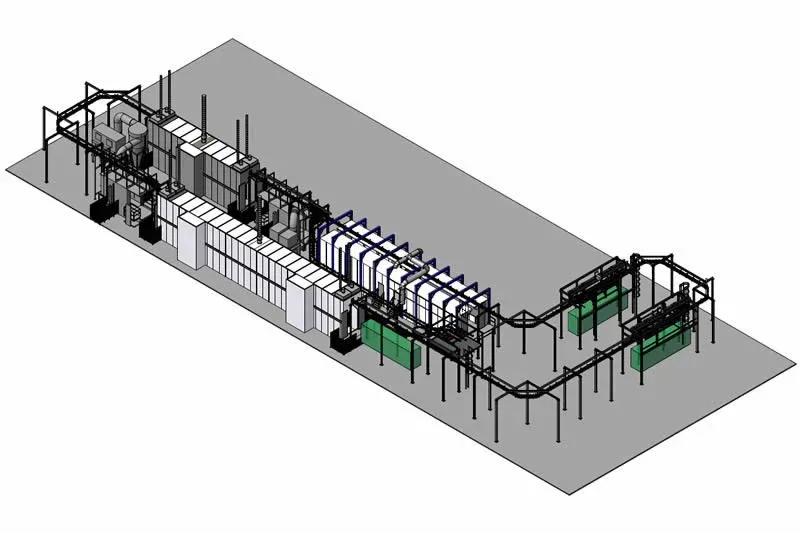
Mechanical Handling Solutions
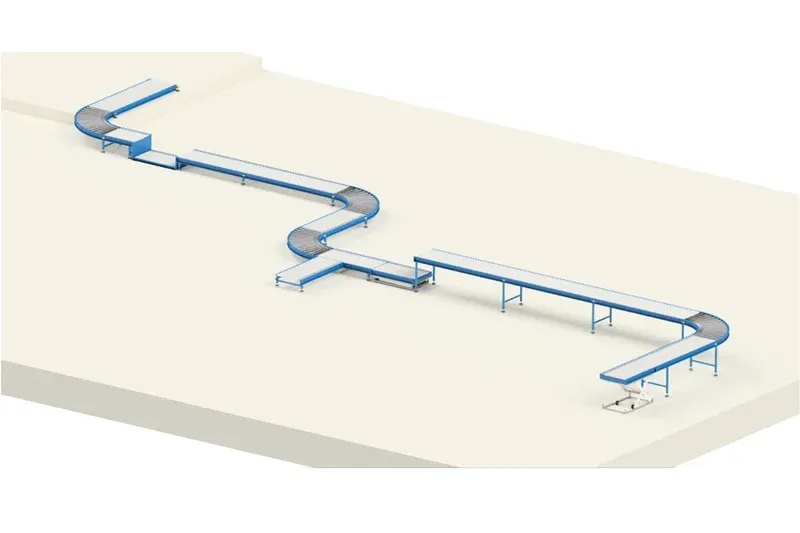
Amber Industries brings together specialist product and service divisions, including MCM Conveyor Systems, Amber Automation, Gramac Quartz Systems, Amber Conveyors and Amber Service. Each division draws on its own engineering expertise, technology and dedicated range of products and services to provide solutions for specific materials handling requirements.
Working individually or together under the Amber Industries Ltd umbrella, these divisions enable us to design and deliver tailored conveyor and mechanical handling solutions for a wide range of applications, from individual items of equipment to complex integrated systems for manufacturing, warehousing and distribution operations.