Multi-million Pound Overhead Conveyor System Nearing Completion
7
Amber Industries are nearing completion of an "AT100 power and free overhead conveyor system", which is part of a multi-million euro expansion program by a key international automotive components supplier. The success of a Power & Free conveyor system lies in it’s flexibility of operation, allowing the flow of product to be controlled with the correct sequencing taking place to suit a customers individual and specific requirements and working environment.
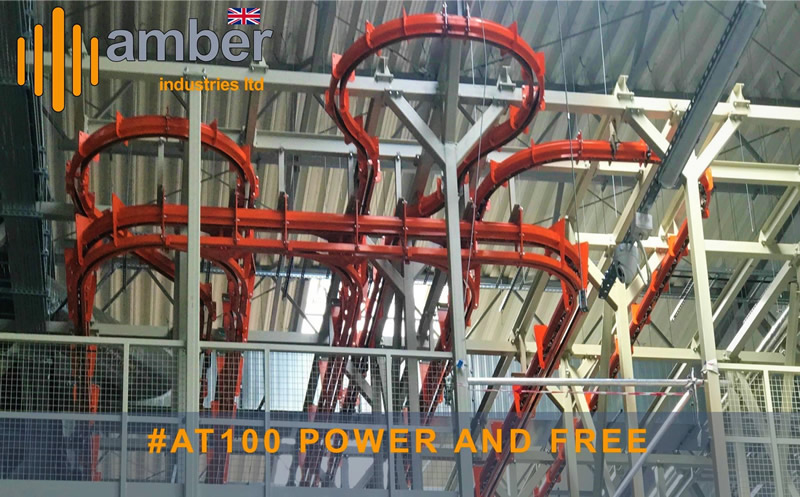
Unlike conventional continuous running chain conveyors, where product loads are attached directly to the conveyor chain via jigs/attachments etc. a Power & Free system utilises a series of free running trolley assemblies, which may be connected together with the use of a flight bar, to carry the load. The trolley assemblies are routed in a twin channel section and driven around the system dependant upon the application by a single or multiple conveyor chains, which are mounted above the twin track/trolley track section. By utilising a trolley assembly to carry a product load, total flexibility, due to the unrestricted movement of the trolley assembly throughout the system can be achieved.
Other Articles
Amber Industries Supports Specialist UK Manufacturer With Conveyor Maintenance Contract
23
MCM Autotrack Conveyor Project For Automotive Components Manufacturer
16
Amber Industries Delivers Conveyor Solution For Street Furniture Manufacturer
12
MCM Sidetrack Monorail Conveyor Systems – Heat Treatment
23
Amber Industries Puts Intelligent Control At The Heart of Conveyor Automation
21
MCM Freetrack Conveyor Systems Providing A Flexible Materials Handling Solution
4
MCM Dualtrack Inverted Conveyor System Delivers Stable & Precision Product Handling
9
Autotrack 500 Conveyor System Upgrade Phase 1 Shipped
26
MCM Sidetrack Monorail Conveyor Systems In Focus
7
That Is A Wrap On Paint Expo 2026
24