Complete Turnkey Floor Conveyor System Project
1
Amber industries recently designed, manufactured and installed a complete bespoke floor conveyor system incorporating ZLP roller conveyors, PLC controls system, product display monitors, barcode scanning, operator interface for product identification in assembly zone. You will see from the image that this is a multi-function floor conveyor installation to meet the requirements of our UK based customer.
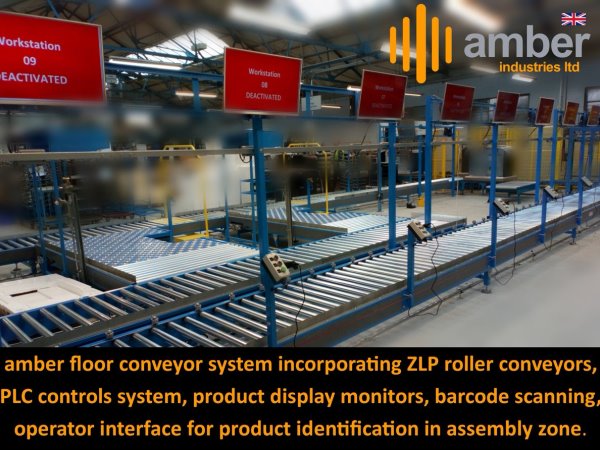
Automated floor conveyor systems are extensively used in warehouses, distribution centres, parcel sorting depots, and all kinds of factory environments; anywhere where unit loads need to be moved. Amber Automation is the division of Amber Industries Ltd. which specialises in automated floor conveyor systems. Our aim is to supply floor conveyor systems precisely tailored to our client’s present and future business needs.
Other Articles
New Lineshaft Conveyor System Enhances Distribution Operations For Global Beauty Product Organisation
30
Amber Industries Supports Specialist UK Manufacturer With Conveyor Maintenance Contract
23
MCM Autotrack Conveyor Project For Automotive Components Manufacturer
16
Amber Industries Delivers Conveyor Solution For Street Furniture Manufacturer
12
MCM Sidetrack Monorail Conveyor Systems – Heat Treatment
23
Amber Industries Puts Intelligent Control At The Heart of Conveyor Automation
21
MCM Freetrack Conveyor Systems Providing A Flexible Materials Handling Solution
4
MCM Dualtrack Inverted Conveyor System Delivers Stable & Precision Product Handling
9
Autotrack 500 Conveyor System Upgrade Phase 1 Shipped
26
MCM Sidetrack Monorail Conveyor Systems In Focus
7